

Water-based inks are pigment or dye systems suspended in water rather than a solvent or plasticiser carrier, and they are the right choice whenever you need a soft hand feel, PVC-free credentials, or a genuinely eco-friendly print on natural-fibre textiles and paper substrates, as explained in the Psychology of colors in marketing. The trade-off is real: they demand more from your press, your dryer, and your operator.
Quick pros:
- Soft, breathable hand feel that sits in the fabric rather than on top of it
- PVC-free and phthalate-free, with significantly lower VOC emissions than solvent systems
- Easy water-based cleanup; no solvent waste to dispose of
- Strong eco credentials supporting REACH and Oeko-Tex compliance
Quick cons:
- Lower opacity on dark garments without high-solids acrylic (HSA) or discharge techniques
- Sensitive to drying in the screen, especially in warm or low-humidity environments
- Curing requires precise airflow as well as heat, typically around 160°C / 320°F
- Switching from plastisol usually means dryer upgrades and operator retraining
Key takeaways
Water-based inks are the right production choice for soft-hand, eco-credentialled apparel and paper printing, but they require precise curing with forced airflow and a press setup that plastisol operators will need to learn.
| Point | Details |
|---|---|
| Best use case | Cotton-rich apparel, premium posters, and sustainable packaging where soft hand and PVC-free credentials are required. |
| Opacity on darks | Standard RFU inks are not sufficient; specify HSA or discharge and run a sample trial on the actual blank before production. |
| Curing is two-stage | Water must evaporate fully under forced airflow before binder cross-linking completes; a forced-air conveyor dryer is essential. |
| UK market is growing | The UK waterborne inks market grew 4.27% in 2024, driven by regulation and sustainability demand, improving stock availability. |
| A3m production support | A3m handles ink specification, sample trials, and washfastness testing for branded apparel and merchandise projects across the UK. |
Table of Contents
- What types of water-based inks are there?
- Where do water-based inks perform best?
- Water-based vs plastisol: advantages and trade-offs
- How do you set up a press for water-based printing?
- Troubleshooting common problems on press
- How to buy water-based inks in the UK
- UK brands and suppliers worth knowing
- What the market data tells UK buyers
- A3m’s perspective on specifying water-based inks
- Bespoke branded apparel and print production with A3m
- Sources
What types of water-based inks are there?
Understanding the ink families before you specify or order saves a great deal of trial and error. Each type suits a different combination of substrate, opacity requirement, and production volume.
-
Ready-for-use (RFU) inks are pre-mixed, low-viscosity systems designed for printing straight from the tub. They work well on light-coloured natural-fibre garments and paper, and they are the most accessible entry point for smaller print runs. The trade-off is modest opacity, so they are not the answer for printing white or bright colours on navy or black.
-
High-solids acrylic (HSA) inks contain a higher proportion of pigment and binder solids, which gives them noticeably better coverage on mid-to-dark grounds. HSA systems and discharge inks are the two main routes to increased opacity on dark garments, though HSA can feel slightly heavier than a standard RFU because more material sits in the fabric. For branded T-shirts where a bright logo must read clearly on a charcoal base, HSA is usually the practical answer.
-
Discharge inks work by chemically removing the reactive dye from the fabric and replacing it with pigment, leaving a print that is genuinely part of the cloth rather than a layer on top. The result is an exceptionally soft hand, but the process only works on 100% cotton garments dyed with reactive dyes. Polyester, nylon, and pigment-dyed blanks will not discharge correctly, so substrate verification is non-negotiable before specifying this system.
-
Medium and low-solids inks sit between RFU and HSA in terms of pigment load. They are commonly used for halftone and process-colour work on light grounds, where their lower viscosity helps them hold fine detail through higher mesh counts without bridging or flooding.
-
Speciality aqueous and hybrid water-based UV inks cover a broader range of substrates including coated papers, board, and some flexible packaging films. Hybrid water-based UV systems cure under UV rather than heat, which changes the equipment requirements entirely but opens up non-porous surfaces that standard water-based inks cannot reliably bond to.
Quick selection guide:
- Light cotton apparel, small runs: RFU
- Bright or white on dark cotton: HSA or discharge
- Soft vintage feel on 100% reactive-dyed cotton: discharge
- Fine halftone or process colour on light grounds: medium/low solids
- Coated board or flexible packaging: aqueous or hybrid UV
Where do water-based inks perform best?
The primary home for water-based screen printing inks is natural-fibre textiles, and for good reason. Cotton and cotton-rich blends absorb the water carrier, allowing the pigment and binder to penetrate the fibre structure rather than sitting on the surface. The result is a print that moves with the garment, breathes naturally, and survives repeated washing without the cracking that can affect thick plastisol deposits.
Primary application categories:
- Branded apparel: T-shirts, hoodies, tote bags, and workwear where a soft, retail-quality finish is the brief. Water-based inks are the standard choice for fashion-led brands and sustainable merchandise ranges.
- Premium posters and art prints: Water-based systems on uncoated or lightly coated paper deliver rich, matte colour with no plastic sheen, which is why they dominate fine-art and gig-poster production.
- Sustainable packaging and folded cartons: On uncoated board and kraft stock, water-based inks support recyclability and are compatible with many food-safe certification pathways. For more on how this works in practice, A3m’s guide to sustainable packaging print covers the key considerations.
- Soft signage and fabric displays: Exhibition banners, retail fabric displays, and event backdrops printed on polyester-blend fabrics often use dye-sublimation rather than screen printing, but water-based systems are used for shorter runs on natural-fibre soft signage where sublimation is not appropriate.
Substrate caveats worth knowing:
- Polyester and synthetic blends resist water absorption, which reduces ink penetration and can cause dye migration (the garment’s own dye bleeding into the ink layer). Specialist low-bleed or polyester-specific water-based formulations exist, but they add complexity.
- Coated films and non-porous surfaces generally need a primer or a switch to a UV-curable or solvent system. Standard water-based inks will not adhere reliably without surface preparation.
- Dark-coloured garments of any fibre type need HSA or discharge to achieve acceptable opacity, as covered in the types section above.
Pro Tip: Before committing a dark-garment job to a standard RFU ink, always request a strike-off on the actual blank. Opacity looks very different on a digital proof versus a printed swatch on a navy 280gsm fleece.
Water-based vs plastisol: advantages and trade-offs
Choosing between water-based and plastisol inks comes down to aesthetic versus production needs, and neither system wins on every axis. The table below sets out the key dimensions side by side.
| Dimension | Water-based | Plastisol |
|---|---|---|
| Hand feel | Soft, breathable, in-fabric | Sits on surface; can feel rubbery at heavy deposits |
| Opacity on darks | Moderate (HSA/discharge needed) | Excellent straight from the tub |
| Eco credentials | PVC-free, phthalate-free, low VOC | Contains PVC and plasticisers |
| Curing | Heat + airflow; ~160°C / 320°F | Heat only; more forgiving temperature window |
| Screen sensitivity | Higher; dries in screen if left | Lower; stays open longer |
| Cleanup | Water and mild detergent | Requires solvent ink degrader |
| Washfastness | Excellent when fully cured | Excellent |
| Cost per litre | Often higher | Generally lower |
Operational considerations you should plan for:
- Throughput: Water-based inks can slow production on manual presses because operators need to flood the screen between pulls to prevent drying. Automatic presses with short cycle times manage this better.
- Training: Operators moving from plastisol need hands-on time with flood-stroke technique, retarder use, and dryer settings. Expect a learning curve of several production runs before consistency improves.
- Waste-water handling: Rinsing screens produces pigment-laden water. UK trade effluent regulations may require a settlement tank or filtration before discharge to drain, depending on your local authority’s consent conditions.
- Pricing impact: Higher ink cost and longer cure times can affect job pricing, particularly on short runs. Factor in the premium before quoting.
Switching from solvent or plastisol to water-based systems reduces VOC emissions and improves workplace safety, but it typically requires investment in drying technology and material testing before production volumes are reliable.
How do you set up a press for water-based printing?
Getting the press right is where most problems either start or get solved. Water-based inks are less forgiving of sloppy setup than plastisol, but a well-configured press produces results that plastisol simply cannot match on feel.
Mesh selection
Mesh counts for general water-based printing typically run from 110 to 160 threads per inch (TPI), with fine-detail work going up to 225 TPI. Lower mesh counts (86–110 TPI) suit heavy HSA deposits or underbase layers; higher counts (180–225 TPI) are for halftone and process-colour work where ink laydown must be thin and precise.
| Application | Recommended mesh (TPI) |
|---|---|
| HSA underbase / heavy deposit | 86–110 |
| General water-based printing | 110–160 |
| Fine detail / halftone | 180–225 |
Emulsions and screen care
Use a water-resistant dual-cure or SBQ-based emulsion for water-based printing. Standard diazo emulsions soften and break down quickly when exposed to water-based inks, particularly on longer runs. Coat screens to a slightly higher EOM (emulsion over mesh) than you would for plastisol, as this helps ink release cleanly and reduces pinholes.
Between pulls, always flood the screen with ink to keep the mesh wet. If you are stopping for more than a few minutes, cover the screen or print a few test sheets before resuming. Modern formulations and correct press technique, including water-resistant emulsions and consistent flood strokes, have significantly reduced early drying-in problems, but process discipline remains the deciding factor.
Curing: the two-step process
Curing water-based inks is a two-stage event, not a single pass through heat.
- Evaporation: Heat and forced airflow remove the water carrier from the ink film. This must happen completely before cross-linking can begin. Insufficient airflow at this stage causes steaming, where trapped moisture prevents the binder from setting properly.
- Cross-linking: Once the water has left, the binder cures at temperature, typically around 160°C / 320°F, locking the pigment into the fibre structure.
Forced-air conveyor dryers are the industry standard for water-based inks because they remove evaporated moisture reliably. A heat tunnel without active airflow will steam the print rather than cure it, producing poor washfastness even when the surface appears dry. For high-volume production, a dual-pass method through the dryer (a flash station to evaporate, then a full conveyor pass to cross-link) gives the most consistent results.
Pro Tip: Run a wash test on your first production batch, not just a finger-rub check. Wash the test garment at 40°C and inspect for fading or cracking before committing the full run to the dryer settings you have chosen.
Essential equipment checklist
- Forced-air conveyor dryer with adjustable belt speed and temperature zones
- Flash cure station for dual-pass or underbase work
- Squeegees with a medium-to-hard durometer (70–80 shore) for clean ink shear
- Water-resistant dual-cure or SBQ emulsion
- Retarder additive on hand for warm-weather or slow-press situations
Troubleshooting common problems on press
Even a well-set press throws up problems. Here are the most frequent issues and how to address them quickly.
Drying in the screen
- Cause: Ink drying in the mesh between pulls, particularly in warm rooms or with slow press speeds.
- Fix: Flood the screen immediately after each pull. Add a water-based retarder (typically 2–5% by weight) to slow open time. Lower room temperature if possible, or mist the screen lightly with water between pulls on manual presses.
Poor opacity on dark garments
- Cause: Standard RFU or low-solids ink used where HSA or discharge is needed.
- Fix: Switch to an HSA formulation or, on 100% reactive-dyed cotton, use a discharge base. Print a white HSA underbase first, flash, then overprint the colour.
Undercure and poor washfastness
- Cause: Insufficient airflow in the dryer, belt speed too fast, or temperature too low.
- Fix: Reduce belt speed to extend dwell time. Check that the dryer’s air jets are clear and functioning. Verify temperature with a donut probe or heat-sensitive tape at the garment surface, not just the dryer display.
Ghosting or halo around the print
- Cause: Moisture migrating outward during curing, or discharge activator spreading beyond the print area.
- Fix: Reduce discharge activator concentration. Increase airflow to draw moisture straight up rather than outward. Check that the garment is not damp before printing.
Colour shift after washing
- Cause: Undercure, or a mismatch between the ink system and the garment’s dye chemistry (common with discharge on incompatible blanks).
- Fix: Confirm full cure with a wash test. Verify that the blank is 100% reactive-dyed cotton if using discharge. Switch to HSA if the blank chemistry is uncertain.
Pre-press quick checklist:
- Mesh tension checked and within specification
- Emulsion fully hardened and water-resistant
- Room humidity below 60% where possible
- Dryer airflow confirmed operational before the run starts
- Retarder and binder additives available at the press
- Test garment washed and inspected before full production begins
How to buy water-based inks in the UK
Buying well means asking the right questions before the ink arrives, not after the first failed wash test. Here is what to request from any supplier.
Specification checklist:
- Solids percentage and recommended mesh range
- Cure profile: temperature, belt speed, and required airflow
- Washfastness data (number of washes at what temperature)
- REACH compliance confirmation and any Oeko-Tex certification
- Substrate compatibility list (cotton, poly-cotton, paper, board)
- Recommended emulsion type and EOM
- MSDS / safety data sheet
Typical pack sizes and pricing shape:
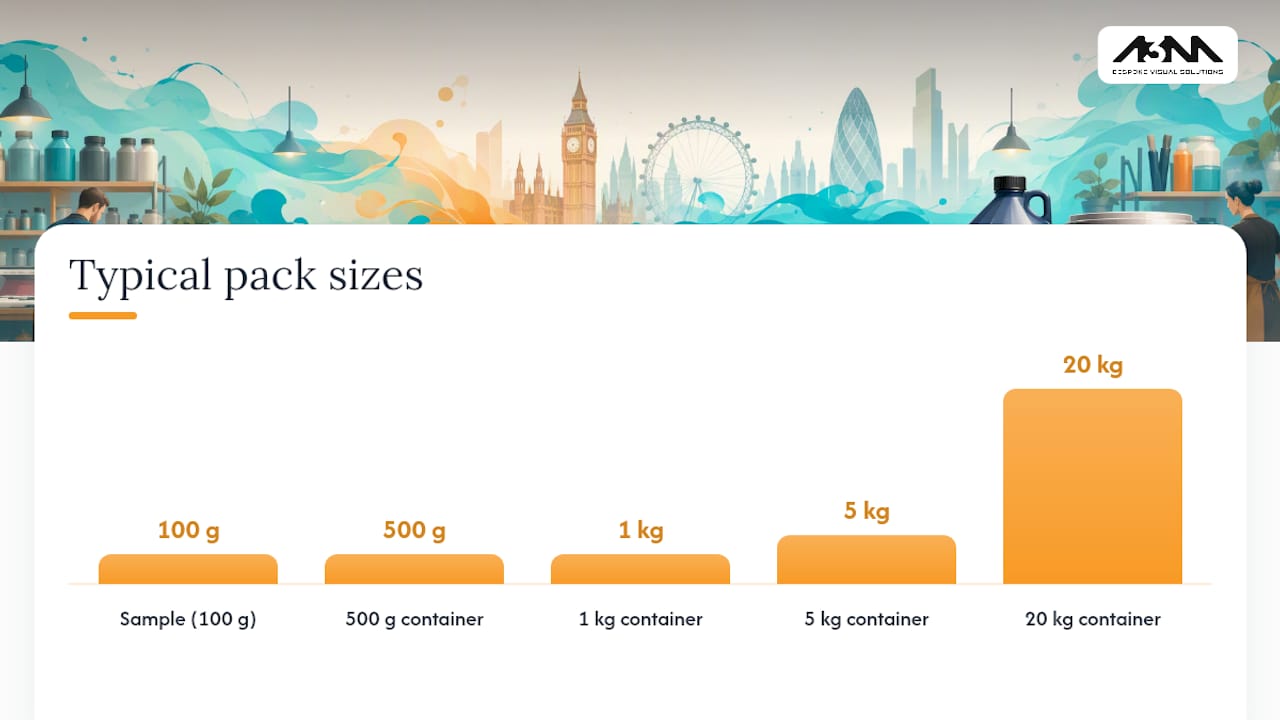
Water-based inks for screen printing are commonly available in 500g, 1kg, 5kg, and 20kg containers. Sample or trial packs (typically 100g–500g per colour) are widely offered by UK trade distributors and are worth requesting before committing to a full production quantity. Pricing varies considerably by formulation: HSA and discharge systems tend to cost more per kilogram than standard RFU inks, reflecting the higher pigment load and more complex chemistry.
Questions worth asking your supplier:
- Can you provide a sample print on the actual blank I am using?
- What underbase do you recommend for this ink on this substrate?
- What is your lead time for trade quantities, and do you hold stock in the UK?
- Is technical phone or email support available if I hit curing problems?
Evaluating sample packs:
Print the sample on your intended blank, cure it through your actual dryer at your planned settings, then wash it three times at 40°C before assessing opacity, hand feel, and colour accuracy. A sample that looks good straight off the press but fades after one wash tells you the cure profile needs adjustment, not that the ink is poor.
For teams evaluating in-house print production, running a structured sample trial before switching ink systems is the single most reliable way to avoid costly production errors.
UK brands and suppliers worth knowing
The UK market has a solid range of water-based ink brands available through trade distributors, with most offering sample quantities and technical datasheets on request.
-
Permaset (Colormaker Industries): a well-established range of water-based screen printing inks widely used for apparel and textile applications. Known for good washfastness and a broad colour palette, with PVC-free and Oeko-Tex-certified options. Available through UK trade distributors in small and trade quantities.
-
Sericol (Texcharge): Sericol’s Texcharge range is a discharge-based water-based system designed for soft-hand printing on cotton. It is a recognised name in UK trade screen printing and is typically available through specialist distributors rather than general print suppliers.
-
Permaprint: a UK-available range covering both standard water-based and HSA formulations. Often cited by UK printers for its balance of opacity and soft hand on cotton and cotton-rich blends.
-
Ecotex: positioned explicitly as an eco-friendly ink range, Ecotex products are PVC-free and phthalate-free, with a focus on sustainable print production. A practical choice for brands that need to evidence their environmental credentials to clients or retailers.
-
Wicked Printing Stuff (WPS): a UK-based trade supplier stocking a range of water-based inks alongside emulsions, mesh, and press consumables. WPS is known among UK screen printers for accessible pricing, sample availability, and practical technical support.
-
Screen Print World: a UK trade distributor carrying water-based ink lines alongside a broad range of screen printing consumables. Useful for sourcing small sample quantities and comparing formulations side by side before committing to a supplier.
Practical buying hints: always request the technical datasheet and cure profile for any ink before ordering. For discharge or HSA systems, ask specifically whether the supplier can provide compatibility notes for the blank brands you use most frequently. Most UK distributors will arrange a small sample print if you supply your own blanks.
What the market data tells UK buyers
The UK liquid waterborne printing inks market recorded a 4.27% growth rate in 2024, reversing a period of contraction between 2020 and 2023. The drivers are environmental regulation and rising demand for sustainable printing across flexible packaging, labels, and apparel. For procurement teams, this shift has a practical implication: more UK distributors are actively investing in water-based stock and technical support, which means better availability and shorter lead times than were typical five years ago.
Regulatory and sustainability signals to watch:
- PVC-free requirements are increasingly written into retailer and brand sustainability policies, making water-based inks the compliant default for many apparel contracts
- VOC reduction targets under UK environmental regulations continue to push converters and trade printers away from solvent systems
- REACH and Oeko-Tex certification requests from end clients are becoming standard in apparel and promotional merchandise briefs
- Advances in HSA formulations have narrowed the performance gap on opacity and washfastness, making water-based inks viable for a wider range of production types than was the case a decade ago
For teams building a sustainable print production strategy, the market direction is clear: water-based systems are moving from a specialist choice to a mainstream expectation in branded apparel and sustainable packaging.
A3m’s perspective on specifying water-based inks
The conversation about water-based inks that we have most often with clients is not “should we use them?” but “which formulation, on which blank, through which process?” That shift in the question tells you something important: the technology has matured to the point where the decision is no longer ideological. It is operational.
At A3m, we evaluate every branded apparel and merchandise project against substrate, required finish, volume, and lead time before recommending an ink system. Water-based inks are our preferred route for cotton-rich garments, tote bags, and any brief where the client’s sustainability policy requires PVC-free certification. For jobs where opacity on dark grounds is the primary requirement and the blank chemistry is uncertain, we will often recommend an HSA system or a structured trial before committing to discharge. The sustainable print options we offer for events and branded environments, follow the same logic: the right system for the job, specified correctly from the start.
What clients can expect from us during sampling and trials is straightforward: we run the print on the actual blank, cure it through our production dryer, wash-test it, and share the result before any volume commitment is made. No surprises at delivery.
Bespoke branded apparel and print production with A3m
For marketing managers and procurement leads who need a production partner rather than a supplier list, A3m offers bespoke merch and apparel production with in-house capability across water-based, discharge, and specialist print systems. The concrete difference from sourcing ink and running production yourself is that we handle substrate verification, ink specification, sample trials, and washfastness testing as part of the project, not as extras you have to chase.

We work with hospitality brands, retailers, events teams, and commercial clients across the UK, and we are happy to start with a small trial run before any volume commitment. If you have a brief for branded apparel, sustainable merchandise, or printed displays and you want to talk through the right print method for your job, get in touch with the A3m team for a technical conversation and a no-obligation sample quote.
Sources
The following resources cover market data, technical cure guidance, and UK trade supply for water-based inks.
- Choosing the right ink for every job — Printwear & Promotion
- Water-based screen printing ink 101 — Screen Print Direct
- Screenprinting