


$0.08–$0.60 extra: Soft touch lamination for UK print buyers
Soft touch lamination is a thin polymer film with a micro-textured coating that gives paper or board a velvet-like feel, and it’s the fastest way to signal premium quality on packaging or brochures. It suits inner boxes, folding cartons and presentation collateral that people handle and admire. The trade-off: that same soft surface shows scuffs and fingerprints more readily than gloss or standard matte, so it’s the wrong choice for anything travelling loose in a delivery van.
TL;DR:
- Soft touch lamination is best suited for inner boxes, folding cartons, and presentation materials that are handled frequently and need a tactile luxury impression.
- Its vulnerability to scuffs and fingerprints makes it unsuitable for shipping cartons, heavily handled retail displays, or environments with rough transit.
- Achieving optimal results requires matching film thickness, substrate weight, and finishing sequence, with proofs essential to ensure color accuracy and texture.
- The added cost ranges from $0.08 to $0.60 per unit, influenced by coverage area, run length, and additional finishing processes like foil or embossing.
- Advances in recyclable and durable formulations are emerging but do not eliminate the need for careful handling, storage, and pre-production testing to prevent common defects.
Table of Contents
- What is soft touch lamination and how does it differ from matte and gloss?
- Why designers and brands choose soft touch
- When soft touch lamination is the wrong choice
- Technical specifications and production considerations
- What does soft touch lamination cost per unit?
- How to specify soft touch lamination for a project
- A3M practitioner perspective on proofing and real production
- Maintenance and cleaning tips for soft touch laminated products
- Common issues and troubleshooting during the lamination process
- Advances and innovations in soft touch lamination technology
- Why soft touch still gets specified wrong
- Get your soft touch finish specified and produced properly
- Sources
What is soft touch lamination and how does it differ from matte and gloss?
Soft touch lamination uses a polymer film, usually PET or Biaxially-Oriented Polypropylene (BOPP), coated with a micro-textured layer that mimics suede or velvet under the fingertips. The film typically runs 12 to 18 microns thick, thin enough to keep the substrate flexible but dense enough to hold that tactile grip once bonded.
Two bonding methods dominate production. Thermal lamination fuses the film to the printed sheet using heat and pressure through a roller system, which most UK trade finishers run as standard. Adhesive lamination uses a wet or solvent-based bonding agent, better suited to certain heavier boards or when a thermal press isn’t available. Either way, the result behaves very differently to matte or gloss on press:
- Gloss reflects light directly, boosting colour saturation and giving that classic “shiny” print look.
- Standard matte scatters light evenly, flattening reflections and softening colour contrast slightly.
- Soft touch absorbs more light than either, deepening blacks and dark tones while producing almost no reflection at all, which is why it reads as so much more expensive under retail lighting.
That light absorption is doing more work than people assume. It’s not just texture. Dark, high-coverage artwork genuinely looks richer under soft touch than under a standard matte laminate, which is exactly why so many premium beauty and spirits brands specify it for outer sleeves.
Why designers and brands choose soft touch
Soft touch lamination earns its keep at the unboxing moment. It’s the finish that makes a customer pause and run their hand across a box before they open it, and that tactile pause is doing genuine commercial work: soft touch delivers a stronger perception of premium value than matte in many direct-to-consumer and beauty contexts, often for only a modest per-unit increase.
It also plays exceptionally well with other finishing techniques. Foil stamping against a soft touch background creates a striking contrast between matte softness and metallic sheen, and embossing reads far more three-dimensional when the surrounding surface absorbs light rather than reflecting it. Designers should factor that combination into the finishing budget early, since stacking foil or emboss onto soft touch adds to the total per-unit cost.
The applications where this finish earns its premium:
- Inner boxes and rigid presentation cartons that get picked up and inspected.
- Folding cartons for beauty, spirits and confectionery where shelf appeal drives the sale.
- Premium brochures, portfolios and presentation folders handed over in client meetings.
Pro Tip: If you’re combining soft touch with foil, ask your finisher to run the foil stamp after lamination, not before. Foiling through the laminate film gives a cleaner edge and stronger metallic contrast than foiling the sheet first.
When soft touch lamination is the wrong choice
Soft touch has one well-known weakness: it marks. Anything that travels loose in transit, gets stacked in a warehouse, or passes through dozens of hands at a trade show will pick up visible scuffs faster on soft touch than on gloss or an anti-scuff matte laminate. That’s the finish showing scuffs and fingerprints more readily in heavy-contact retail environments than either alternative.
Dark colours make the problem worse. Fingerprints and scuff marks show up more clearly against deep, heavy-coverage inks, which is awkward given how often soft touch gets specified precisely because it deepens dark artwork. Protecting high-contact zones with a spot gloss or foil panel is the usual fix.
There’s a sustainability angle too. As a polymer film bonded to paper or board, soft touch laminate complicates recycling in the same way any plastic film lamination does, and mixed-material packaging generally needs specialist recycling streams rather than standard paper waste.
- Avoid soft touch on outer shipping cartons or anything handled roughly in distribution.
- Use spot gloss or foil to shield logos and text areas prone to fingerprint marks.
- Flag the recyclability question early if the brand has environmental packaging commitments.
Technical specifications and production considerations
Getting the technical brief right up front saves a reprint. Three variables decide how a soft touch job actually performs once it leaves the press, starting with the choice of paper roll supplier that ensures compatible and high-quality substrate availability.
- Film thickness. Most soft touch laminates run between 12 and 18 microns. Thinner films at the lower end feel softer and drape more naturally over flexible stock; thicker films add rigidity and slightly more scuff resistance, useful on folding cartons that need structural stiffness.
- Stock weight and substrate. Lamination films bond best to coated or uncoated stock above roughly 250gsm; lighter sheets can wrinkle or curl once film tension is applied. Checking your packaging board grade against the finisher’s minimum recommended weight avoids that problem before print run day.
- Finishing sequence. Foil stamping, embossing and spot UV should generally be applied after soft touch lamination rather than before, since the film needs a clean substrate to bond evenly. Discuss sequencing with your finisher at brief stage, not after plates are cut.
Getting this sequence backwards is one of the most common and expensive mistakes in premium packaging production.
What does soft touch lamination cost per unit?
Soft touch lamination typically adds between $0.08 and $0.60 per unit, and where you land in that range depends on format, coverage area and run length. A small folding carton with partial coverage sits at the lower end; a larger rigid box or full-wrap application with total surface coverage pushes towards the top of the range.
Set-up costs matter more than most buyers expect. Short runs absorb the fixed cost of tooling and press set-up across fewer units, so per-unit price drops sharply once a run passes a few thousand pieces. If you’re layering foil or embossing on top, budget that as a separate line: combining finishes raises the total per-unit cost beyond the lamination adder alone, sometimes substantially depending on foil coverage area.
How to specify soft touch lamination for a project
A clear brief prevents most soft touch problems before they reach the press. Work through this before you send artwork to a finisher:
- Define the touchpoint. Who handles this item, how often, and under what conditions? Match the finish to the touchpoint and transit conditions rather than choosing on looks alone.
- Map the journey. Inner packaging opened once at the counter behaves very differently to an outer carton stacked in a pallet for three weeks.
- Set the visual goal. Decide whether dark tone depth or foil contrast is the priority, since that shapes ink coverage decisions.
- Confirm the budget ceiling. Know your per-unit target before the quote arrives so you’re not choosing finishes you can’t afford at volume.
- Request colour compensation notes and a physical proof. Soft touch changes perceived saturation compared with a digital proof, so never approve final stock sight unseen.
Pro Tip: Ask your supplier one question before signing off: what rub-resistance grade does the film carry? A vague answer, or a supplier who can’t produce a physical sample on your actual stock, is a red flag worth walking away from.
Reviewing your large format print finish options alongside this checklist helps if you’re specifying finishes across a wider print run, not just packaging.
A3M practitioner perspective on proofing and real production
We always insist on a physical proof under the final stock and finish before committing to a full run. It’s the only reliable way to see how soft touch will actually behave on your artwork, since screens and digital mock-ups never show scuff risk or true colour depth.
We’ve applied soft touch across exhibition collateral and premium gift packaging, where the tactile lift consistently justifies the spend. On material choice, we weigh recyclability against durability needs project by project, steering clients towards the lightest film that still meets their handling requirements.
Maintenance and cleaning tips for soft touch laminated products
Soft touch surfaces need gentler handling than gloss, but they’re not fragile if you follow a few basics. Fingerprint oil is the main enemy, and it sits visibly on the surface rather than soaking in, so regular handling during storage or display gradually dulls the finish.
For everyday cleaning, a soft, dry microfibre cloth removes light dust and surface marks without abrading the texture. Avoid anything abrasive: paper towels, rough cloths and household cleaning sprays containing alcohol or ammonia can strip the micro-texture coating or leave permanent streaking. If a mark needs more than a dry wipe, a barely damp microfibre cloth followed immediately by a dry one usually lifts it without saturating the film.
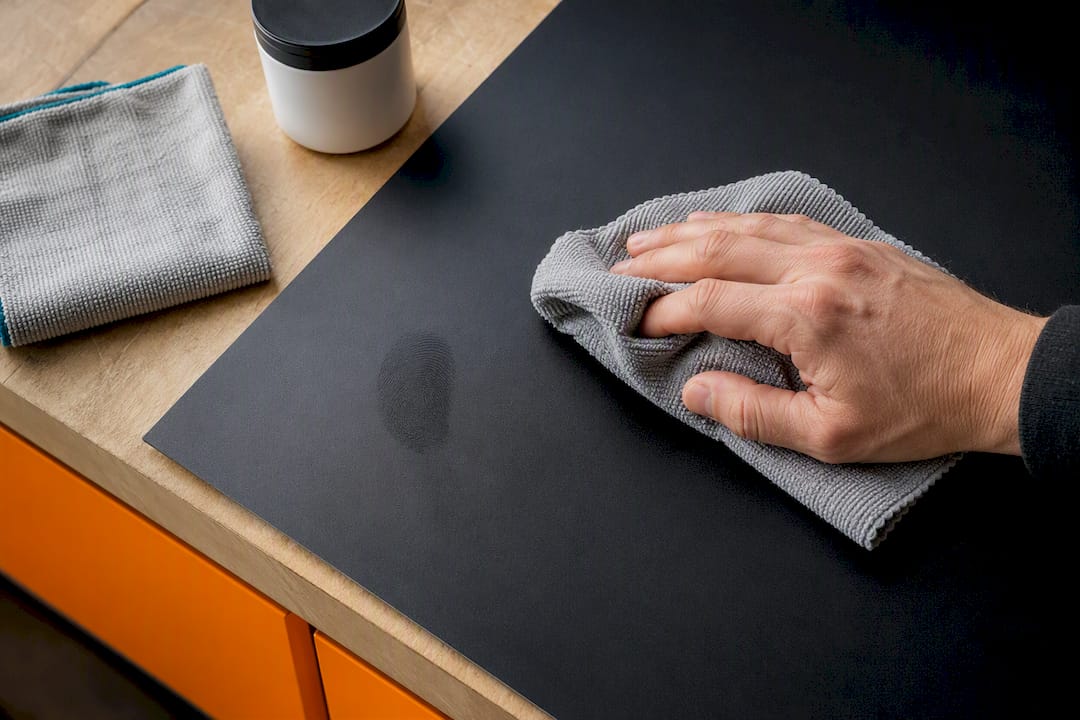
Storage conditions matter as much as cleaning technique. Keep finished stock flat, away from direct sunlight and humidity swings, since polymer films can react to heat by softening slightly, which makes them more prone to picking up marks from whatever they’re stacked against. Interleaving tissue between finished pieces during storage or transit is a simple habit that prevents surface-to-surface transfer marking, especially on dark artwork where every scuff is visible.
For point-of-sale displays or retail packaging that stays on shelf for weeks, brief your team or retail partner on basic care: no adhesive labels applied directly to soft touch panels (they can lift the coating on removal), and no stacking heavy items directly on laminated surfaces. These are small operational details, but they’re the difference between packaging that still looks premium after a month on shelf and packaging that looks tired within days.
Common issues and troubleshooting during the lamination process
Most soft touch problems trace back to one of three causes: substrate mismatch, sequencing errors, or moisture.
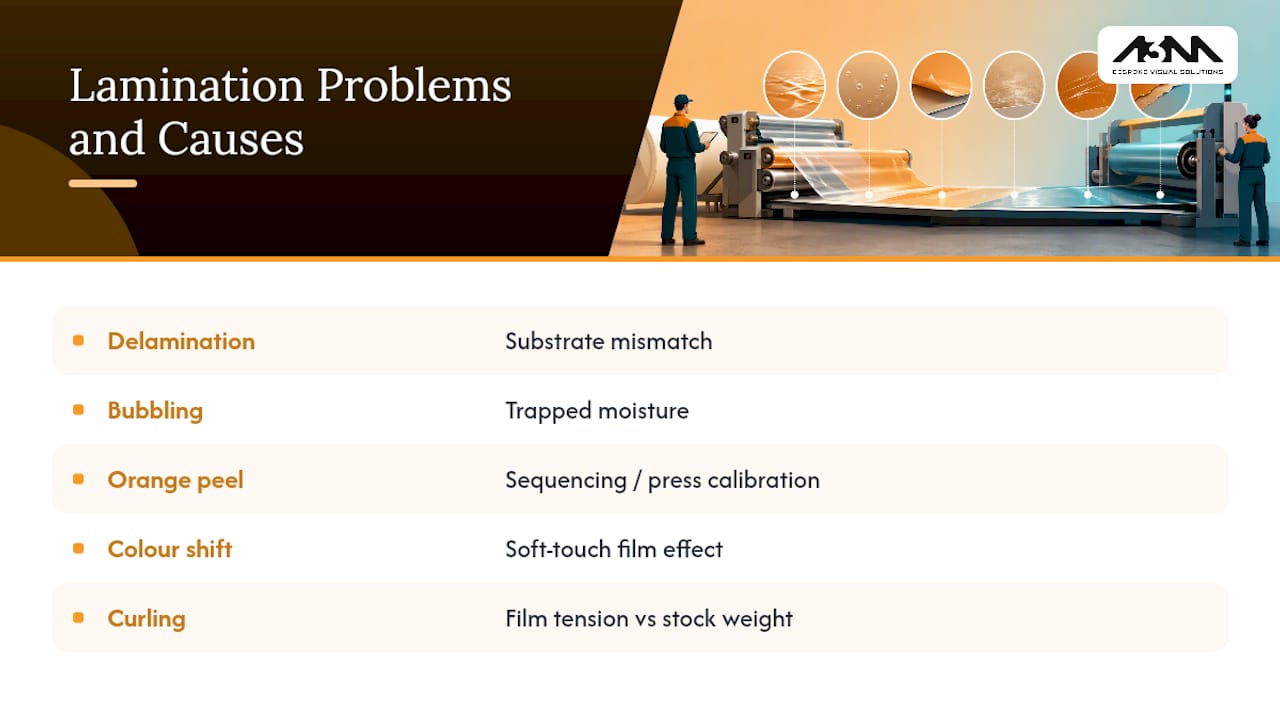
Delamination, where the film lifts or bubbles at the edges, usually points to insufficient stock weight or a substrate with a coating that resists adhesive bonding. If you’re seeing edge lift consistently, check your board grade against the finisher’s minimum recommended weight before blaming the film itself.
Orange peel texture, an uneven, dimpled surface rather than a smooth velvet finish, often results from incorrect roller temperature or pressure during thermal lamination. This is a press calibration issue on the finisher’s side rather than a film defect, and it’s exactly the kind of flaw a physical proof catches before a full run commits to it.
Colour shift is the most commonly reported surprise. Soft touch laminate darkens and mutes colours compared with how they appear on an uncoated proof, which is precisely why digital previews mislead buyers so often. Ink that looked vibrant on screen can read flat and heavy under soft touch, particularly with lighter pastel tones that lose some vibrancy under the film’s light-absorbing texture.
Curling after lamination, where sheets bow rather than lying flat, typically signals a mismatch between film tension and stock weight, more common on lighter substrates under 250gsm. Moisture is the other common culprit: stock stored in humid conditions before lamination can trap moisture under the film, leading to bubbling weeks after production that wasn’t visible at the time of finishing. Storing substrate in a controlled, dry environment before it reaches the press solves this more often than any adjustment to the lamination process itself.
Advances and innovations in soft touch lamination technology
The biggest shift in soft touch technology over recent years has been the push towards recyclable and bio-based films. Manufacturers have been developing polymer alternatives designed to biodegrade or integrate more easily into standard paper recycling streams, addressing the sustainability concern that has historically been soft touch’s biggest drawback against uncoated or varnished alternatives.
Anti-scuff and enhanced rub-resistance formulations are the other major development. These modified coatings aim to retain the velvet hand-feel while improving resistance to the fingerprint and scuff marking that has limited soft touch to lower-contact applications. Early versions trade off slightly on the ultimate softness of the texture, but for brands wanting the tactile signal on items that see more handling, the durability gain often justifies that small compromise.
Digital and hybrid finishing presses have also improved consistency. Newer thermal lamination lines offer tighter temperature and pressure control, reducing the orange peel and uneven bonding issues that plagued older equipment, particularly on shorter runs where a press hadn’t fully stabilised before the job began.
Water-based and low-solvent adhesive systems are gaining ground too, driven partly by environmental regulation and partly by brand demand for lower-impact production. These systems still achieve reliable bonding on most coated stocks, though they can be less forgiving on unusual substrates, which is worth flagging with your finisher if you’re specifying an uncommon board grade.
None of these developments have displaced the fundamentals. A physical proof still catches problems no innovation has fully solved, and thickness, substrate compatibility and finishing sequence still decide most outcomes.
Why soft touch still gets specified wrong
The conventional wisdom treats soft touch lamination as a purely aesthetic upgrade, something you add if the budget allows and skip if it doesn’t. That framing misses the point. Soft touch is a functional decision about who handles the item and how often, and treating it as a style choice is exactly how brands end up with scuffed, fingerprint-covered packaging within a week of hitting shelf.
The advice that gets underweighted most is the physical proof. Buyers routinely approve a digital mock-up and only discover the colour shift or the scuff pattern once the full run is printed and boxed. That’s an expensive lesson to learn twice, and it’s entirely avoidable for the cost of a single proof run.
If there’s one priority worth fixing first, it’s asking the transit and handling question before the aesthetic one. Where does this item travel, and who touches it between the press and the customer’s hands? Answer that honestly, and the choice between soft touch, matte or a hybrid anti-scuff finish becomes obvious rather than a guess made on mood boards.
— Steve
Get your soft touch finish specified and produced properly
A3M is the direct route to soft touch lamination done right, from film specification through to finish stacking with foil or embossing, all handled in-house rather than passed between subcontractors. That in-house control is what lets us hold to the proofing discipline this article has argued for throughout: nothing goes to full production until you’ve seen and felt it on your actual stock.

Whether you’re specifying inner packaging for a product launch, presentation folders for a pitch, or premium collateral for an exhibition stand, our team handles the technical decisions around film thickness, substrate compatibility and rub-resistance so you don’t have to guess. Explore our large format print manufacturing capabilities to see the finishing options available, then get in touch to request a physical sample or a production quote for your project.
Sources
- Soft Touch Lamination for Packaging: When It Works, When It Doesn’t, and What It Costs | Logic Pac
- Soft Touch Finishing in Packaging: What It Is, What It Costs, When to Use It - Crateform
- Matte vs Gloss vs Soft-Touch Lamination Finishes | PackageTheWorld
Recommended
- Wall graphics cost UK: 2026 price guide for businesses
- Water-based inks: the complete UK guide for 2026
- Brochure paper weight: choose the right GSM for print
- Trade show logistics print: a UK procurement guide


UK floor graphics: insist on 36+ PTV and in situ test certificates
For UK workplaces and public spaces, specify floor graphics with a wet-condition pendulum test value (PTV) of 36+, and never rely on an R-rating alone. Insist on an in-situ pendulum test certificate before sign-off, plus a written maintenance plan. That single requirement does more to protect people, and you, than any other line in a spec.
TL;DR:
- Ensure floor graphics in wet areas have a pendulum test value of 36+ and obtain an in-situ pendulum test certificate before sign-off.
- R-ratings are unreliable for wet slip risk; rely on Pendulum Test Value results, especially for installed graphics.
- Reputable labs report the lowest in-situ PTV after bonding, as wear and cleaning often reduce slip resistance over time.
- Certified pendulum testing, using calibrated rubber sliders and water contamination, is the preferred method for UK compliance.
- Regular re-testing and proper installation, cleaning, and maintenance are essential to maintain slip safety standards.
Table of Contents
- What UK floor graphics slip ratings actually mean
- Standards and test methods worth knowing
- Where floor graphics belong, and where they don’t
- What to ask manufacturers before you specify
- Installation and maintenance that protect your slip rating
- Legal duties and how testing supports compliance
- A3m’s perspective on specifying safe floor graphics
- The industry’s blind spot on floor graphics
- Why A3m is the practical choice for compliant floor graphics
- Sources
What UK floor graphics slip ratings actually mean
Two systems dominate UK slip-resistance conversations, and they measure quite different things. The DIN ramp test rates surface from R9 to R13, with R9 covering the lowest resistance and R13 the highest, typically for oily industrial floors. It’s a useful shorthand from manufacturers, but the HSE’s technical guidance flags a real problem: a single R-rating band can span a wide range of actual friction values, so products with the same R rating may behave differently underfoot when wet.
The pendulum test measures something more specific: how a rubber slider, weighted and swung to mimic a heel strike, grips a wet surface. The result is the Pendulum Test Value, and the HSE interprets it plainly: 0 to 24 means high slip potential, 25 to 35 is moderate, and above a certain threshold is classed as low. That’s why UK specifiers lean on PTV rather than R-ratings for wet-slip risk.
Why does the pendulum win out for British conditions? It replicates the hydraulic uplift a heel creates on a wet floor, which the UK Slip Resistance Group notes is far closer to how real slips happen than a static ramp angle.
For floor graphics specifically:
- R-ratings tell you almost nothing about wet-slip behaviour once a film is applied
- PTV testing on the actual installed graphic, not just the base laminate, is what regulators and insurers respect
- A graphic can carry a good R-rating on paper and still test poorly once fitted with print and lamination layers
Standards and test methods worth knowing
British specifiers need to recognise a handful of named methods when reading a lab report. Get familiar with these before you approve any floor graphic:
- BS 7976 / BS EN 16165: the pendulum test standard, operated with a calibrated rubber slider swung across the wet or dry surface. It’s the method HSE prefers for UK risk assessment.
- DIN 51130: the German ramp method behind R9 to R13 ratings, useful for comparing broad product categories but weak on wet-slip precision.
- Rz microroughness: a measure of surface texture depth in microns. The HSE’s GEIS2 guidance treats readings below 10 microns as high slip potential in wet pedestrian areas, 10 to 20 microns as moderate, and above 20 microns as low, using it alongside pendulum results rather than instead of them.
One point catches specifiers out repeatedly: ex-factory PTV figures rarely match what you get once a graphic is bonded to a real floor, grouted around, or scrubbed a few dozen times. Reputable labs report the lowest in-situ PTV recorded, not the best one, precisely because that’s the figure that matters when someone’s shoe meets the floor on a wet Tuesday.
Where floor graphics belong, and where they don’t
Floor graphics earn their place in plenty of commercial settings, but the wrong location turns a marketing asset into a liability.
Environments that work well:
- Dry retail aisles and till points, where footfall is high but contamination is rare
- Exhibition halls and event floors, provided spills are managed quickly
- Office reception areas and corridors with controlled foot traffic and no external weather ingress
- Warehouse and route-marking applications away from vehicle turning zones or oil spill risk
Environments to avoid or approach with serious caution include permanently wet areas, ramps and sloped walkways, commercial kitchens, and exposed entrance zones where rain gets tracked in on shoes. Constant contamination, rolling loads from trolleys or pallet trucks, and mixed footwear all erode the margin a graphic’s slip resistance was tested against.
As a baseline, treat 36+ PTV in both wet and dry states as the minimum for general low slip potential, and push higher for transport hubs, station concourses, or anywhere with heavy footwear and constant footfall.
Pro Tip: If an entrance zone genuinely needs branding, consider a combination of matting and signage rather than a floor graphic. A well-placed site safety board can carry the message without sitting directly in the wet-shoe path.
What to ask manufacturers before you specify
Procurement teams often accept a supplier’s headline rating without asking for the paperwork behind it. Don’t. Demand the following as standard:
- The in-situ PTV, not just a laboratory or ex-factory figure
- The slider type used (four-S rubber is the UKSRG-recommended standard)
- The contamination medium used during testing (water is standard for most commercial floors)
- The test date and the testing body’s accreditation
- Expected PTV degradation over a defined wear cycle
Two broad material categories dominate the market: textured one-part self-adhesive films, and two-part systems combining a printed film with a separate anti-slip laminate. The two-part route generally holds slip performance for longer under heavy foot traffic, though it costs more upfront and needs more careful installation.
Industry guidance recommends annual in-situ pendulum testing in high-traffic zones, because foot traffic and cleaning chemicals both degrade PTV over time, sometimes dropping a floor from an acceptable rating to a risky one within a year or two.
Build your tender documents around these checklist items: required PTV threshold, slider and contamination method, warranty period against slip degradation, and a written re-test schedule. A supplier who can’t answer these without hesitation isn’t ready for a commercial contract. A3m’s product range is specified with exactly this evidence trail in mind.
Installation and maintenance that protect your slip rating
A graphic that tested well on the bench can still fail on site if installation or upkeep is sloppy. Get the fundamentals right from day one:
- Prepare the substrate properly: dust, grease, and old adhesive residue all compromise bond strength and let moisture creep under the edges.
- Seal every edge: peeling corners aren’t just untidy, they’re a trip hazard and a route for contamination to sit beneath the film.
- Set a cleaning regime: use only cleaning agents the manufacturer approves; harsh degreasers and steam cleaning can strip texture faster than normal wear.
- Respond to spills immediately: matting near entrances and quick-response spill protocols matter more for floor graphics than for bare flooring, since the printed surface can mask early wear.
- Re-test annually in high-traffic zones, and immediately after any slip incident, following the post-incident testing practice that professional testers recommend.
Pro Tip: Photograph the installation on day one and again at each maintenance check. A simple before/after record, alongside your test certificates and cleaning logs, is often the single most persuasive piece of evidence in a liability discussion.
Legal duties and how testing supports compliance
Regulation 12 of the Workplace (Health, Safety and Welfare) Regulations 1992 requires floors to be suitable, in good condition, and free from hazards that could cause a slip. It doesn’t set a numeric slip rating. There’s no legal figure written into statute.
That gap is exactly why HSE and UKSRG guidance functions as the de facto industry benchmark. Courts and insurers look for evidence that a dutyholder acted reasonably, and a PTV of 36+ backed by a dated test certificate is far stronger evidence than a manufacturer’s marketing claim.
- Keep every pendulum test certificate on file, dated and signed
- Log cleaning schedules and spill responses as they happen, not retrospectively
- Bring in an accredited tester for any change of use, high footfall increase, or after an incident
- Talk to your insurer early if you’re specifying graphics for a public-facing or transport-adjacent space
A3m’s perspective on specifying safe floor graphics
A3m manufactures large-format print in-house, which means slip testing evidence gets built into a project from the design stage, not bolted on afterwards. We ask every material supplier for the same paperwork we’d expect a client to ask us: in-situ PTV, slider type, contamination medium, and test date.
At handover, clients receive a short pack: the test certificate for the specific product used, manufacturer cleaning guidance in plain language, and a suggested inspection schedule tailored to footfall. That’s not a sales gimmick, it’s what keeps a floor graphic doing its job six months after installation, not just on the day it’s laid.
The industry’s blind spot on floor graphics
Most guidance on slip resistance treats floor graphics as an afterthought bolted onto general flooring advice, and that’s a mistake. A plain vinyl floor and a printed, laminated graphic on top of it are not the same surface, even when the base substrate is identical. The print layer, the lamination, the adhesive bond at the edges: each one changes the friction profile, and none of that shows up if you only ask for the base material’s R-rating.
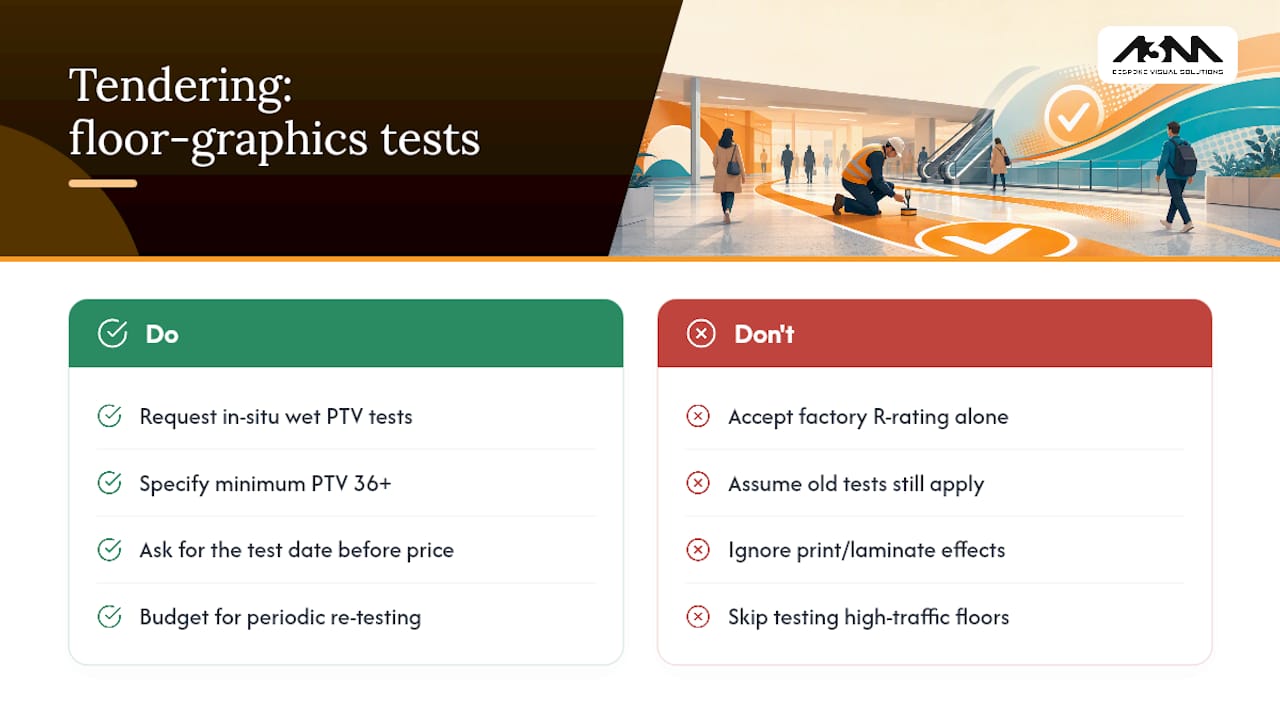
The uncomfortable truth is that plenty of floor graphics get specified on a manufacturer’s headline number alone, with nobody checking whether that number reflects the installed product, in situ, under wet conditions. HSE’s own guidance is explicit that ex-factory figures can diverge sharply from real-world performance once a floor has been grouted, polished, or simply walked on for a few months. Treat that divergence as the rule, not the exception, and budget for re-testing rather than assuming day-one performance holds forever.
If there’s one habit worth building into every tender, it’s this: ask for the test date before you ask for the price. A PTV of 36+ from three years ago on a heavily trafficked floor tells you almost nothing useful.
— Steve
Why A3m is the practical choice for compliant floor graphics
A3m gives UK facilities and procurement teams something most print suppliers don’t: in-house manufacturing that keeps slip-testing evidence attached to the product from design through to installation, rather than chasing a third-party supplier for paperwork after the fact.
Where a generic print vendor might hand over a graphic with a manufacturer’s generic R-rating and little else, A3m builds the evidence trail into the order itself: in-situ PTV data, slider and contamination details, and a maintenance schedule suited to your footfall. That matters whether you’re branding a retail rollout, an exhibition floor, or a hotel lobby, because the wrong laminate in the wrong location becomes a liability long before it becomes a design problem.
If you’re specifying floor graphics for a UK site and want the testing evidence sorted before installation day, get in touch about A3m’s large-format print manufacturing capabilities and ask for a quote against your specific floor plan and footfall pattern.
Sources
Keep these documents alongside your procurement and handover paperwork: the HSE’s flooring guidance, the GEIS2 technical note on pendulum operation and Rz roughness, UKSRG’s pendulum introduction, and the Workplace Regulations text itself. File test certificates and cleaning logs with every contract, and if you manage a venue rather than a single site, the Jigsaw Conferences guide to venue safety regulations is a useful companion piece for wider site duties.
- HSE: Assessing the slip resistance of flooring
- HSE technical guidance: assessing slipperiness of floors (GEIS2)
- The Workplace (Health, Safety and Welfare) Regulations 1992 — Regulation 12
- UK Slip Resistance Group: Introduction to the pendulum tester
Recommended
- Trade show logistics print: a UK procurement guide
- Window manifestation UK: compliance guide for building managers
- Luxury retail window graphics explained: 2026 UK guide
- Large format print quality check: a production guide

Avoid Failed Press Runs: Hot Foil vs Cold Foil for Designers (3 Questions)
Choose hot foil when you need tactile depth, embossed detail, or reliable results on uncoated and textured stock. Choose cold foil when you need inline metallic colour effects, faster turnaround, and lower per-unit cost on bigger runs. A3m works with both processes daily and can help you test the right one before you commit to a full production run.
TL;DR:
- Hot foil provides a deeper, more reflective metallic finish and is more reliable on uncoated, textured, or fibrous stocks, making it ideal for luxury packaging.
- Cold foil allows for inline processing, quicker turnarounds, and the ability to overprint colors, but performs poorly on uncoated or absorbent stocks.
- Die costs and lead times significantly impact hot foil economics on short runs, while cold foil offers faster setup and lower per-unit costs for larger volumes.
- Combining hot and cold foil in one job is feasible and often used to balance visual impact with cost efficiency, typically with a hot foil logo over a cold foil background.
- Choosing the right process depends primarily on substrate type, run length, and design complexity, with thorough testing on actual stock advisable before full production.
Table of Contents
- Hot foil vs cold foil: the core differences at a glance
- How does hot foil stamping actually work?
- How does cold foil printing work in practice?
- Which stocks and artwork rules suit each foiling method?
- What do tooling and run length do to cost and lead time?
- Can you combine hot foil and cold foil on one job?
- How did we specify foiling for a real packaging brief?
- How do you choose between hot foil, cold foil, and hybrid?
- Why “just pick the cheaper option” is the wrong question
- Get technical support for your next foiling project
- Sources
Hot foil vs cold foil: the core differences at a glance
The mechanical difference decides almost everything else. Hot foil uses a heated metal die, pressed under pressure directly onto the substrate, to transfer foil in a single strike. Cold foil works differently: a UV curable adhesive is printed inline, foil is laminated onto that adhesive, then cured under UV light as the sheet moves through the press.
That single distinction drives every downstream decision, from tooling cost to how the finished piece feels under a thumb.
- Process: hot foil needs a custom die and heat; cold foil runs inline with no die at all
- Setup: hot foil requires die-making lead time; cold foil changes over faster, since there’s no die tooling to wait on
- Finish: hot foil gives denser, more reflective metallic and a raised tactile edge; cold foil gives a flatter metallic that can be overprinted in CMYK
- Substrate: hot foil tolerates uncoated and textured stocks; cold foil prefers smooth, coated surfaces
- Speed and cost: cold foil suits higher volumes at lower per-unit cost; hot foil suits shorter runs where die cost amortises less painfully
Neither process is universally “better”. They solve different problems, and the smartest packaging briefs specify the process based on the job, not on habit.
How does hot foil stamping actually work?
A heated die, engraved with your design, presses foil film onto the substrate under controlled pressure. The heat activates an adhesive layer on the foil, bonding it permanently to the surface it touches. That direct contact under heat and pressure is why hot foil delivers superior metallic density and a genuinely raised, tactile finish that cold foil simply cannot match in a single pass.
It’s also more forgiving on stock choice. Uncoated boards, textured papers, and fibrous packaging materials that would cause cold foil’s adhesive to soak in unevenly take hot foil cleanly, because the die transfers foil mechanically rather than relying on surface energy.
- Works reliably on uncoated, textured, and fibrous substrates
- Produces the deepest, most reflective metallic finish available
- Can combine foil and embossing in the same die pass for a genuine 3D effect
- Best suited to luxury packaging, invitations, and premium short-to-mid runs
Artwork discipline matters here more than most designers expect. Reverse type and fine serif fonts can “fill in” under heat and pressure if the die isn’t engineered with adequate stem width, and a competent die-engineer will often add micro-breaks to protect fine detail. Minimum stroke widths, sensible letter spacing, and early conversations with your die-maker prevent expensive reprints.
Pro Tip: Send your artwork for die-engineering review before finalising layout, not after. A die-engineer can flag fine reverse type or tight tracking that will bridge under heat, saving you a second die cut.
How does cold foil printing work in practice?
Cold foil skips the die entirely. A UV curable adhesive is printed inline in the exact pattern you want foiled, foil film is pressed onto that wet adhesive, and UV light cures the bond as the sheet continues through the press. Because this happens inline, cold foil supports faster press speeds and eliminates a separate handling stage, which matters when your schedule is tight.
The creative upside is real: cold foil lets you overprint CMYK inks directly onto the metallic base, producing colour-shifted foils, metallic gradients, and halftone effects that a single hot foil pass cannot achieve. That’s a genuinely different creative toolkit, not just a cheaper substitute.
- Runs inline with the press, no separate die pass required
- Enables CMYK or PMS overprinting for custom metallic colours and gradients
- Delivers lower per-unit costs on medium-to-large volumes
- Needs smooth, coated stock for consistent adhesion
The trade-off is adhesion sensitivity. Cold foil performs poorly on uncoated or highly absorbent stocks, where the adhesive can soak in unevenly and leave patchy, dull coverage rather than a clean metallic surface.
Pro Tip: If your stock sits anywhere near the borderline between coated and uncoated, run a small trial sheet before committing. Patchy cold foil on a full production run is far more expensive than a wasted proof.
Which stocks and artwork rules suit each foiling method?
Smooth, coated stocks favour cold foil; uncoated, textured, or heavily fibrous stocks push you towards hot foil. That’s the starting rule, but it’s not the whole brief.
- Check surface energy first. Marginal stocks sometimes need an inline primer or varnish station to improve cold foil adhesion, though this adds process complexity and cost worth weighing against simply switching to hot foil.
- Set minimum line weights early. Fine reverse type and thin serifs need wider stems for hot foil dies; cold foil is more forgiving on line weight but less forgiving on colour registration.
- Isolate foil areas from tight knockouts to avoid bridging in either process, and confirm registration tolerance with your supplier before finalising layout.
- Request a press trial on your exact stock and varnish combination, since testing the real substrate before full production catches adhesion problems no spec sheet will predict.
Pro Tip: Include your actual stock sample with any technical brief, not a generic paper description. GSM alone doesn’t tell a printer how it will take foil. Our guide to choosing the right print finish covers this pairing in more depth.
What do tooling and run length do to cost and lead time?
Die cost is the variable that catches people out. A custom hot foil die is a fixed cost that gets amortised across the run, which makes short runs relatively expensive per unit and long runs far more reasonable.
Cold foil flips that logic. There’s no die to pay for or wait on, so setup is quicker and changeovers between jobs are faster.
- Hot foil: higher upfront die cost, longer lead time, cost per unit falls as volume rises
- Cold foil: no die tooling, faster changeover, lower per-unit cost sustained across medium-to-large runs
- Hybrid jobs (both processes on one piece) carry both cost structures, so budget and schedule accordingly
- Always ask your supplier for die lead time separately from press time; the two get conflated too often
If your run length is genuinely uncertain, that ambiguity itself is useful information. It usually points towards cold foil, or towards holding off on a hot foil die commitment until volume is confirmed.
Can you combine hot foil and cold foil on one job?
Yes, and it’s more common than most designers realise. A frequent hybrid pairs a cold foil background, covering a full panel in metallic colour, with a hot foil logo or wordmark stamped on top for tactile emphasis. This combination balances cost against visual depth rather well: the expensive, high-impact element gets the die treatment, while the broad metallic coverage stays cheap and fast.
Separate embossing passes are sometimes unavoidable, particularly when the emboss depth needed exceeds what a single foil die can deliver alongside the foil transfer itself.
- Specify which elements need hot foil versus cold foil clearly in your brief, not just “add foil”
- Request registration proofs between passes, since misalignment between cold foil backgrounds and hot foil detail is the most common hybrid failure
- Ask for scuff and adhesion testing on the finished combined sample, not just the individual processes
- Weigh the visual uplift against the added complexity honestly; not every brief needs both
How did we specify foiling for a real packaging brief?
A recent brief called for premium gift packaging on an uncoated, lightly textured board, with a short run and a strong emphasis on shelf presence. Cold foil was ruled out early because of the substrate; the texture would have caused patchy adhesive coverage.
The board’s texture made the decision for us before cost even entered the conversation. Hot foil gave us clean, dense metallic coverage and let us combine the logo strike with a light emboss in the same die pass, which is exactly the tactile cue premium packaging needs to earn a second look on shelf.
Steve, who leads production decisions like this at A3m, tested the die on sample stock before committing to the full run, catching a minor bridging issue on fine type early enough to correct the die engineering without delaying the job.
How do you choose between hot foil, cold foil, and hybrid?
Three questions settle most specification decisions before you touch a supplier’s order form.
- What’s the substrate? Uncoated or textured stock generally rules out cold foil; smooth coated stock opens both options.
- What’s the run length? Short, premium runs tend to favour hot foil despite die cost; medium-to-large runs favour cold foil’s per-unit economics.
- Do you need tactile depth? If the brief demands a raised, embossed, or richly dimensional finish, hot foil (or a hybrid) is the only route that delivers it convincingly.
Once you’ve answered those three, ask your supplier for the specifics that actually prevent failed runs: a physical proof on your exact stock, adhesion testing if you’re near the coated/uncoated borderline, honest die lead time (not just press time), and scuff resistance testing if the packaging will see handling in transit or on shelf. A supplier who hesitates on any of those four questions is one you should be cautious about handing a full production run to.
Why “just pick the cheaper option” is the wrong question
Most briefs I see treat hot foil and cold foil as a straight cost comparison, and that’s the wrong frame entirely. The real question is whether the substrate and the tactile requirement even leave you a genuine choice. Half the “which foil is cheaper” conversations I’ve been part of evaporate the moment someone checks whether the stock is coated. Get the substrate test done before you get quotes, not after.
— Steve
Get technical support for your next foiling project
A3m runs specialist foil and finishing work alongside our large format print manufacturing, which means hot foil, cold foil, and embossing decisions get made by people who handle the die trials and press runs directly, not passed through a broker.
If you’re specifying a packaging, POS, or branded print job that needs foiling, send us your artwork, intended stock, run length, and the finish effect you’re after, and we’ll advise on the right process before you commit to tooling. Uncertain about substrate suitability? Our team can run a proof on your actual stock rather than a generic sample, which is the single best way to avoid a failed press run. Explore our large format print manufacturing capabilities or get in touch to request a technical consultation and proof for your next foiling project.
Sources
For deeper technical detail beyond this comparison, the sources referenced throughout cover the mechanics and economics of both processes thoroughly: INX International’s guide to foil techniques, Arkay’s packaging foil stamping resource, Robus India’s comparison of key differences, and Crateform’s hot foil versus cold foil breakdown. For substrate selection specifically, our own guide on product packaging print and design partners like Branded Agency’s print and packaging design resource are worth a read too.
- Mastering the Art of Foil Printing: A Complete Guide to Hot and Cold Techniques
- Foil stamping for packaging: Hot foil vs. Cold foil
- Hot foil stamping vs cold foil stamping: Key differences
- Hot foil vs cold foil
Recommended
- How to choose large format print finish
- Print artwork file preparation: the 2026 production guide
- Dieline basics: a practical starter for packaging design

Web-to-print portals: the B2B buyer's guide to smarter print ordering
A web-to-print portal is a cloud-based ordering platform that gives central marketing teams brand control while letting local managers order print on demand. For B2B buyers running multiple sites, that combination solves two problems at once: uncontrolled brand spend and slow, manual ordering. Getting it right, though, depends less on which platform you pick and more on how deliberately you plan the rollout.
TL;DR:
- Most successful web-to-print portals depend on clear internal ownership and defined approval processes before development begins.
- Key features to look for include role-based permissions, template locking, digital proofing, and integration with MIS, ERP, or procurement systems.
- ROI primarily comes from improved brand governance, faster approvals, reduced inventory costs, centralized spend visibility, and scalable templates for multiple sites.
- Internal template loading and stakeholder feedback are common bottlenecks; early planning and staged testing are essential for a smooth rollout.
- Choosing a provider like A3m, which combines manufacturing with portal management, ensures a seamless chain from order to production without quality or lead time issues.
Table of Contents
- What is a web to print portal and how does it work?
- Core features to expect in a modern web-to-print portal
- Business benefits and where the ROI actually comes from
- How to implement a web-to-print portal without it stalling at week six
- How A3m implements web-to-print for multi-site businesses
- Why choose A3M for web-to-print portal projects
- A practical checklist for procurement and operations leads
- Sources
What is a web to print portal and how does it work?
A web-to-print portal sits between three groups: a central marketing or brand team, local managers scattered across sites, and the print supplier fulfilling the orders. The central team builds and locks a library of approved templates. Local managers, whether that’s a hotel front-of-house manager or a franchise operator, log in, pick a template, personalise the parts they’re allowed to change, and send the job to production. No design software, no rogue Word documents, no waiting on a marketing team that’s three time zones and one long email chain away.
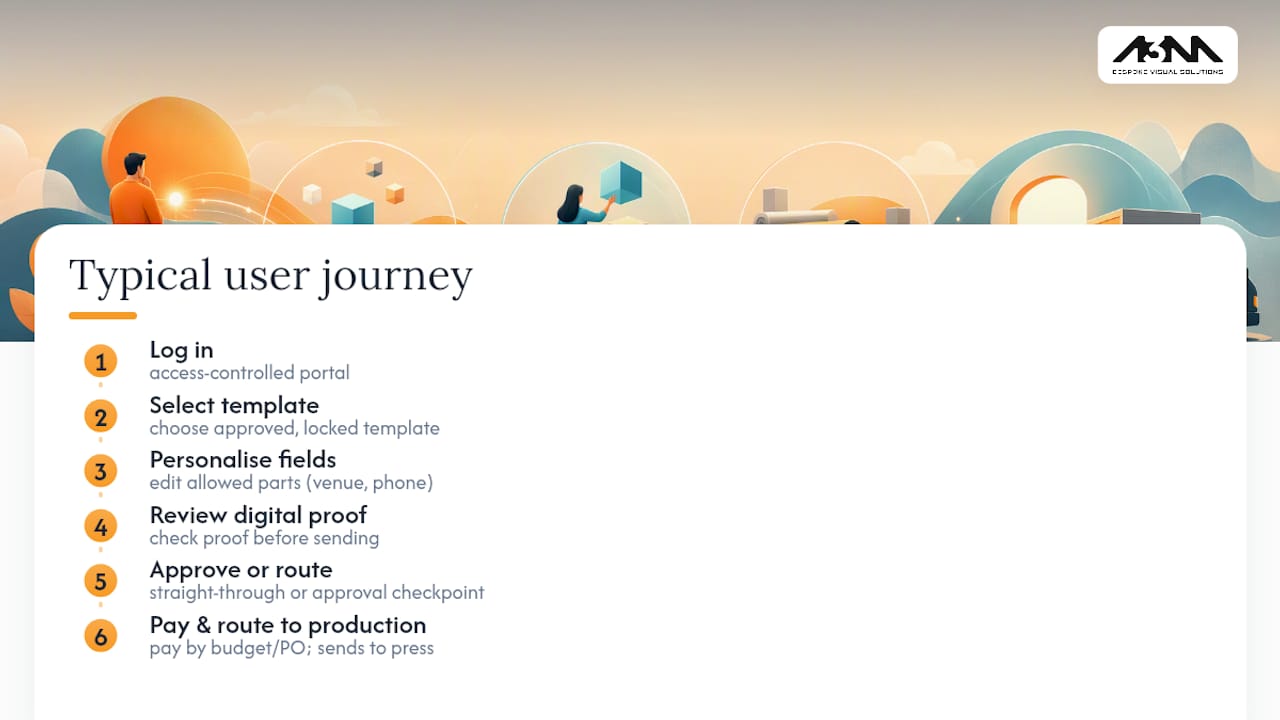
The typical user journey follows a predictable path: log in, select a template, personalise fields like a venue name or local phone number, review a digital proof, approve or route it for sign-off, pay against a budget code or purchase order, and the job routes straight to production. Some platforms build this as a fully automated straight-through process; others insert an approval checkpoint before anything reaches press. Either way, the goal is the same: reducing errors and improving spend visibility across every location ordering from the platform.
It’s worth separating two very different models here. Consumer-facing print shops, the kind where anyone can upload a photo and order a canvas print, optimise for open access and impulse purchase. B2B closed-shop portals do the opposite: they restrict who can order, what they can change, and how much they can spend. B2B web-to-print and corporate print portals centralise templates, enforce brand rules, and grant role-based access precisely so that decentralised ordering doesn’t mean decentralised branding. If your organisation has more than two sites reordering the same signage, POS displays, or stationery, you almost certainly need the closed-shop model, not the consumer one.
Core features to expect in a modern web-to-print portal
Vendor demos tend to sell on visual polish. That’s the wrong lens for a B2B buyer. What actually determines whether a portal earns its keep is a specific set of functional capabilities, and any RFP should test for all of them directly.
- Template libraries with locked fields that let local users edit only pre-approved zones (a name, a date, a local address) while fonts, logos, and layout stay fixed.
- Personalisation and variable-data printing, so a single template can output hundreds of location-specific versions without redesign.
- Digital proofing and preflight checks that catch colour, resolution, and bleed issues before a file ever reaches a press.
- Role-based permissions and approval workflows, including budget controls that stop a site manager exceeding an agreed spend cap without sign-off.
- Order management and reporting, giving procurement a live view of what’s been ordered, by whom, and at what cost, with automatic routing into production queues.
- Integration endpoints covering DAM systems, MIS/ERP platforms, procurement PunchOut catalogues, and payment gateways.
That last point matters more than most buyers initially assume, especially when considering content marketing automation to scale operations. Enterprise-grade web-to-print storefronts typically need to talk to MIS/ERP and procurement systems to support live pricing rules and correct production routing, not sit as a standalone tool bolted onto the side of your operations. Governance features, closed shops, negotiated catalogues, and role-based workflows, are what separate a genuinely useful B2B web to print platform from a glorified upload form, and they’re what enterprises and franchises actually pay for.
Business benefits and where the ROI actually comes from
The financial case for a web-to-print portal rests on five levers, and most organisations underestimate how much they’re losing before they fix them.
- Brand governance: locked templates stop regional teams commissioning their own designs, which is where most rogue print spend originates.
- Faster approvals: digital sign-off replaces email threads and printed proofs sitting in someone’s in-tray.
- Lower inventory costs: print-on-demand removes the need to warehouse boxes of signage or stationery that go out of date the moment a phone number changes.
- Central spend visibility: procurement can see exactly what every site has ordered, rather than reconciling invoices after the fact.
- Scalability: a template built once serves twenty sites as easily as two, which matters enormously for franchise and multisite rollouts.
Pro Tip: Audit your current print spend by site before you build the business case. Most organisations discover at least one category, business cards or POS cards are the usual suspects, where three or four sites have quietly been ordering from three or four different local printers at three or four different price points.
Centralised ordering through a single portal reduces duplicate jobs and improves brand consistency across every location, and gives finance teams a spend picture they simply can’t build from scattered supplier invoices. The governance argument alone tends to justify the investment before cost savings are even factored in, because enterprises and franchises see higher returns when governance is treated as a core deliverable rather than an afterthought.
How to implement a web-to-print portal without it stalling at week six
Most implementation failures aren’t platform failures. They’re planning failures, usually rooted in unclear ownership and feedback that arrives in fragments rather than in one decisive round. Here’s the sequence that actually works.
- Plan. Define template scope, approval hierarchy, budget rules, and integration requirements before any development starts. Decide who owns the project internally, not the vendor, you.
- Execute. Build the environment across three stages: development, staging, and live. This separation matters because it lets your team test changes without risking the production site.
- Populate the storefront. Load templates, product data, pricing rules, shipping options, and payment configuration. This is consistently the heaviest workstream and the one most organisations under-resource, because it depends on internal teams supplying assets on time rather than on vendor speed.
- Pre-launch and UAT. Run real test orders through the full journey, from login to production handoff, on the staging environment. Check role-based permissions actually restrict what they’re supposed to restrict.
- Go live. Switch the storefront live, monitor the first orders closely, and keep a support line open for the inevitable “I can’t find the template I need” questions.
- Onboard. Run a live training session with existing clients or site managers rather than relying on a written guide, and consider incentivising the first few orders to break old ordering habits.
The strongest predictor of an on-time launch isn’t the platform you choose. It’s whether a single internal project owner has been named, with a fixed approval rhythm, before development begins. Most mid-size storefronts launch within a few months when that discipline is in place; the timeline stretches well beyond that when feedback arrives piecemeal from six different stakeholders instead of one accountable decision-maker.
On the technical side, expect a proper baseline: managed hosting, scheduled backups, uptime monitoring, and a security review before go-live. None of this is optional for a B2B deployment handling payment data and brand assets. And don’t skip storefront population, it’s tempting to treat template loading as an afterthought, but it routinely runs in parallel with development and becomes the actual bottleneck when internal teams are slow to supply logos, copy, and pricing.
A quick word on procurement integration: if your organisation already runs purchase orders through a PunchOut catalogue, factor that connection into your RFP from day one. Retrofitting it after launch means rebuilding parts of the commerce layer you thought were finished. For a wider view of how branded print fits into procurement policy, our guide to branded print in procurement covers the compliance angle in more detail.
How A3m implements web-to-print for multi-site businesses
A3m runs web-to-print portals as an extension of in-house manufacturing, not a separate side service. That matters because a portal is only as good as the production capability behind it: when your large format print manufacturing sits under the same roof as your portal fulfilment, there’s one supplier accountable for the whole chain instead of three you’re chasing across different contracts.
Our process for multisite clients follows a consistent pattern:
- Set up dev, staging, and live environments before any templates are loaded, so testing never touches the production storefront.
- Lock templates against brand guidelines first, then build personalisation fields around what local teams genuinely need to change.
- Integrate with existing MIS/ERP and procurement systems early, rather than treating integration as a bolt-on after launch.
- Recommend a named project owner on the client side, with agreed approval turnaround times, before development starts.
- Run staged UAT with real orders, then a live onboarding session for site managers before go-live.
Case studies and client outcomes from specific multisite rollouts are available on request through our exhibition and signage portfolio pages, which show the fulfilment side of the same governance model in practice.
Why choose A3M for web-to-print portal projects
If you’ve read this far, you already know the platform matters less than the discipline behind it, and that’s exactly where A3m earns its place. We combine multisite portal implementation with in-house manufacturing, which means the same team that governs your templates also produces the signage, POS displays, and branded print that comes out the other end. That’s one supplier accountable for the whole chain, not a portal vendor pointing you to a print partner you’ve never spoken to.
Because production sits under our own roof, from large format print to signage and branded environments, there’s no handoff gap where quality or lead times slip. We manage the technical baseline (dev, staging, live, backups, security) and the storefront population work that most rollouts underestimate, so your team focuses on approvals rather than chasing template assets. If you’re weighing up a web-to-print rollout for a multisite estate, get in touch about our large format print manufacturing capabilities and we’ll talk through what a managed implementation would look like for your sites.
A practical checklist for procurement and operations leads
Strip away the vendor pitches and the decision comes down to two things most organisations get wrong first. Appoint a project owner before you sign anything, someone internal who can approve or reject within 48 hours, not a committee that meets fortnightly. Every stalled rollout traces back to feedback arriving in fragments rather than from one accountable person.
Second, don’t launch and hope. Run a live onboarding session with your site managers and offer a small incentive for the first order placed through the new portal. Old habits (calling the local printer, emailing a PDF) are stickier than any feature list, and the platforms that succeed are the ones that get real usage in week one, not week twelve.
— Steve
Sources
Recommended
- Corporate event print ordering: a planner’s guide – A3M
- Common print procurement mistakes businesses make – A3M
- Trade show logistics print: a UK procurement guide – A3M
- The role of branded print in procurement: 2026 guide – A3M

Exhibition stand storage: how to keep displays show-ready
For most exhibitors, professional, exhibit-aware storage is the safest and most cost-effective way to keep stands show-ready between events. Self-storage only makes sense for small, low-cost items like banners and pop-ups. Here’s why the professional route wins for anything modular or custom-built:
- Graphic protection: climate control and proper hanging stop warping, delamination and colour fade.
- Lower repair costs: fewer reprints and panel replacements between shows.
- Simpler move-in: components arrive inspected, labelled and ready to build.
Your next step is straightforward: document a full intake inventory of your stand, then choose the storage option that matches its value and complexity.
Key Takeaways
Professional, exhibit-aware storage protects graphics and structural components, cuts repair and reprint costs, and keeps move-in predictable when providers manage it as active lifecycle care rather than static warehousing.
| Point | Details |
|---|---|
| Choose storage by asset value | Use exhibit-house storage for modular or custom stands; self-storage only for small, low-value items. |
| Document everything at intake | Photograph condition, log every component, and confirm portal access before handover. |
| Pack for the next build | Reverse-order packing with a setup diagram inside each case cuts delays at the next venue. |
| Book retrieval three weeks out | This window allows time for inspection, repairs and repacking before move-in. |
| Verify insurance and red flags | Confirm custody and transit cover in writing, and avoid providers without condition reporting. |
Table of Contents
- What professional exhibition stand storage actually covers
- Which storage option suits your exhibition stand?
- How do you pack and store an exhibition stand properly?
- How do you choose a good exhibition stand storage provider?
- What does exhibition stand storage cost and how far ahead should you book?
- A production partner’s view on stand storage
- Why treating storage as passive warehousing is a costly mistake
- Sources
What professional exhibition stand storage actually covers
A proper storage programme isn’t a lock-up with your name on the door. It’s active management of an asset that has to perform on demand.
Providers running a genuine service typically offer:
- Itemised intake with photographs and written condition notes for every panel, frame and case.
- Climate control, CCTV monitoring, and fire or pest protection built into the facility.
- Barcode or RFID tracking with a client portal showing where each item sits and when it’s due out.
- Pre-show staging, inspection and minor refurbishment before the stand ships.
Providers commonly run itemised intake with photos, condition reports, barcode or RFID tracking, and client portals precisely because exhibition assets move constantly and get handled by different crews each time. Without that paper trail, nobody can prove whether damage happened in transit, on site, or in storage. A well-run programme also schedules pre-show inspection and refurbishment into the storage window itself, so faults get fixed while the stand is idle rather than discovered the morning of move-in.
Which storage option suits your exhibition stand?
Three models dominate the market, and each carries a different balance of cost, risk and effort.
- Exhibit-house storage — the builder or a specialist exhibition storage partner holds your stand, usually with climate control, inventory tracking and pre-show prep bundled in.
- Commercial warehouse storage — general-purpose logistics space, sometimes climate-controlled, but rarely staffed by people who understand exhibition hardware.
- Self-storage units — cheap, flexible, and suitable only for small or low-value kit.
The trade-offs break down like this:
- Exhibit-house storage costs more monthly but protects graphics, LEDs and fabricated structures properly, and it usually includes reassembly support.
- Commercial warehousing sits in the middle: reasonable environmental control, but you handle inventory and prep yourself.
- Self-storage is the cheapest option upfront, yet modular and custom exhibits risk warping, delamination and LED failures without proper humidity and temperature control.
Choose exhibit-house storage for anything custom-built or graphics-heavy. Commercial warehousing works for simple modular kits with in-house handling capacity. Reserve self-storage for banners, pop-ups, and low-value literature stands.
How do you pack and store an exhibition stand properly?
Teardown is where most damage happens, not transit. Rushed packing at 11pm on the last day of a show is how frames get scratched, cables go missing and graphics crease. Follow a consistent sequence every time.
- Photograph everything before packing. Capture condition on every panel, frame joint and lighting rig while it’s still on the show floor.
- Pack in reverse setup order. The last thing you’ll need to install first should sit on top of the case.
- Tape a setup diagram inside each case lid. Packing in reverse order with a diagram inside the case prevents build delays at the next venue, because nobody has to guess which bracket goes where.
- Bag and label every fixing. Screws, connectors and brackets go into labelled bags, taped directly to their parent component, not loose in a box.
- Handle graphics correctly. Roll fabric graphics on cores rather than folding them, and store rigid panels flat or vertical in foam-lined cases, never leaning under weight.
- Check electrical components at intake. Remove and label power supplies, and test LED drivers before they go into storage, not the night before the next show.
- Build a master manifest. List every structural piece, graphic panel, hardware bag and case number, with a photo per box where possible.
Pro Tip: Keep a laminated copy of the setup diagram inside every case and a digital copy in your storage provider’s portal. If a case goes astray, you can rebuild from the diagram alone.
How do you choose a good exhibition stand storage provider?
Ask direct questions before signing anything. A provider’s answers here tell you more than their brochure ever will.
- What does your intake procedure look like, and do I get an itemised condition report with photos?
- Is there a web portal so I can check inventory and shipment status myself?
- What are your climate-control specs, and do you have sprinklering, fire suppression and CCTV in place?
- Can you refurbish or repair panels in-house, and what’s your lead time for pre-show staging?
- How is pricing structured, cubic footage or service tier, and are there minimum terms or notice periods?
- What’s covered under your insurance while my stand is in your custody or in transit, and what’s excluded?
Red flags are easy to spot once you know what to look for: no condition reporting at intake, vague or verbal insurance assurances, and no offer of pre-show inspection. If a provider can’t answer the portal or insurance question clearly, treat that as a decision point, not a detail to chase later. Where you’re relying on public reviews to shortlist providers, check how those reviews are collected and verified, since platform review policies vary and case studies or direct references tell you more than a star rating.
What does exhibition stand storage cost and how far ahead should you book?
Monthly storage costs vary mainly with size, whether climate control is included, and how much service sits on top of basic space. A small modular kit in unclimatised warehouse space costs far less than a large custom stand in a fully monitored, climate-controlled facility with inventory management and portal access.
Timing matters just as much as price. Requesting your storage pull at least three weeks before move-in gives enough runway for inspection, minor repairs and repacking. Compress that window and you’re paying for rush shipping or emergency repairs instead.
A few cost drivers worth flagging:
- Climate-controlled space and service-level extras (staging, inspection, refurbishment) push monthly rates up.
- Exhibit-house storage often costs more per month but lowers total cost of ownership by avoiding repeat repair and reprint spend.
- Insurance matters in both directions: check declared-value cover for transit and separate custody limits while the stand sits in storage.
- Emergency pulls with short notice typically carry a premium over standard retrieval lead times.
A production partner’s view on stand storage
Storage works best when it’s part of the same process that built the stand. A3m’s bespoke exhibition stand builds are designed with reassembly and repair in mind from the outset, and our Vector service supports that lifecycle between shows.
An integrated partner cuts the number of handoffs between build, storage and staging, which shortens pre-show lead times. When you commission a stand, ask your builder for a proper handover pack: full inventory, setup diagrams, and maintenance notes for hardware and graphics.
Why treating storage as passive warehousing is a costly mistake
Most exhibitors still think of storage as a place to put things, not a process that protects them. That’s the real gap in how this topic gets handled. A stand isn’t a static object between shows; it’s a set of materials that degrade, hardware that loosens, and electronics that fail quietly if nobody checks them.
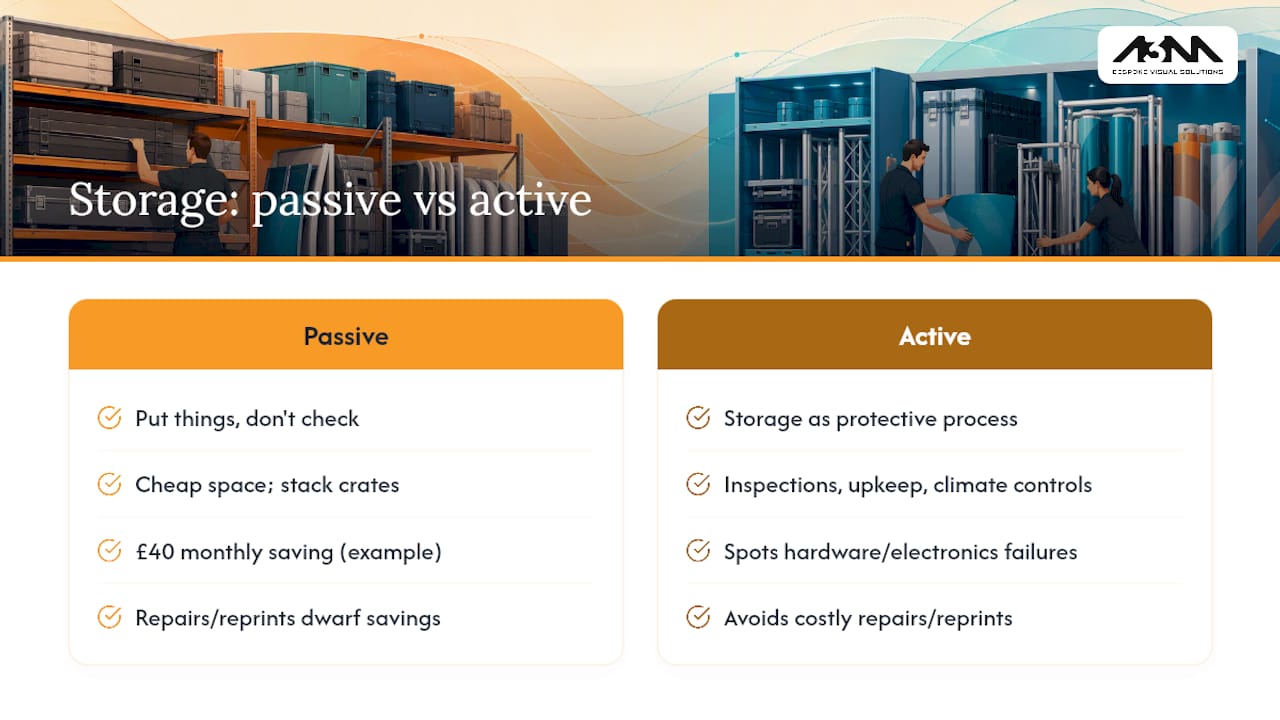
The conventional advice, find cheap space and stack the crates, ignores the fact that repair and reprint costs almost always dwarf the storage saving. A £40 monthly difference between a basic unit and a climate-controlled facility means nothing next to a £2,000 graphic reprint caused by damp.
What should you prioritise first? Documentation. Not the fanciest facility, not the smartest barcode system, just a clear photographic and written record of what you own and what condition it’s in. Everything else, climate control, portals, pre-show staging, only works once you know exactly what you’re protecting. Get that right and the rest of the decision becomes far easier.
— Steve
Sources
- Trade show storage: How to store your exhibit between shows
- Exhibition storage guide: How to store stands & displays between shows
Recommended
- Bespoke Exhibition Stands – A3M
- Exhibition stand lighting: the complete UK buyer’s guide – A3M
- The Ultimate Guide to Illuminated Exhibition Displays: Maximising Trade Show Impact – A3M

Do you need local authority signage permission in the UK?
You probably need advertisement consent if your sign is bigger than 0.3 square metres or illuminated in any way. Smaller, non-illuminated signs and short-term notices under 0.6 square metres often fall under deemed consent, meaning you can display them without applying, provided you stay within strict size, position and mounting rules. The only way to be certain is to check your specific case against the Planning Portal’s advertisement guidance and speak to your local planning authority before you order anything.
Here’s what to do before you commission a sign:
- Check whether your proposed sign fits a deemed consent class on the Planning Portal
- Confirm you have the landowner’s written permission, not just your own lease
- Ask your local planning authority whether the site sits in a conservation area or area of special control
- Establish whether the sign sits near a highway boundary, which may need separate authority sign off
Key Takeaways
Getting local authority signage right in the UK means matching your sign against the 0.3 square metre and illumination thresholds before you order anything, then confirming landowner and highway permissions in parallel with your planning application.
| Point | Details |
|---|---|
| Check the core thresholds | Signs over 0.3 square metres or any illuminated sign usually need express consent. |
| Know your consent route | Deemed consent applies automatically to qualifying classes; express consent needs a formal application. |
| Budget for fees and timescales | Expect £174 for business/advance signs or £610 for other adverts, with decisions within 8 weeks. |
| Only two tests apply | Local authorities can only refuse on amenity or public safety grounds, never commercial need. |
| Prepare full paperwork early | Location plans, scaled elevations and landowner permission prevent the most common delays. |
| Work with a signage specialist | A3m designs and produces signage built around local authority amenity and safety requirements from the outset. |
Table of Contents
- What counts as local authority signage under UK rules
- Is it deemed consent or express consent?
- What do councils actually weigh up when deciding?
- Your checklist for applying for advertisement consent
- What happens if you get it wrong
- What A3m sees business owners get wrong on signage compliance
- The gap between planning theory and what actually gets refused
- Get your signage designed right the first time
- Sources
What counts as local authority signage under UK rules
An “advertisement” in planning law is far broader than most business owners expect. It covers any word, letter, model, sign, placard, board, notice, device or representation used for advertisement, announcement or direction, and that includes far more than the fascia sign above your shop door.
The types business owners encounter most often are:
- Fascia signs fixed flat against the shopfront, usually showing the trading name
- Projecting or hanging signs that stick out perpendicular to the building
- Hoardings used around construction sites or temporary developments
- Pole and totem signs standing free of the building, common at retail parks and forecourts
- Flags and banners used for promotions or seasonal trading
- Estate agent boards and advance or directional signs pointing customers to a location
Some categories draw far more scrutiny than others. Illuminated signs of any size, gable-end adverts painted or mounted on the side of a building, fascia signs mounted above 4.6 metres, and large poster hoardings are the sign types most likely to need express consent. At the other end of the scale, a small name or number plate identifying the occupier, and temporary notices up to 0.6 square metres displayed for a limited period, typically sit within an exempt or deemed consent class. If you’re unfamiliar with the terminology, A3m’s guide to what signage actually means is a useful primer before you dig into the regulations.
Is it deemed consent or express consent?
Deemed consent means the sign is automatically permitted because it fits a class set out in the regulations, without you filing an application. Express consent means you have to submit a formal application to your local planning authority and wait for a decision. Getting this distinction wrong is the single most common reason business owners end up in dispute with their council.
Under the Town and Country Planning (Control of Advertisements) (England) Regulations 2007, deemed consent classes come with strict conditions attached, covering size, position, illumination and how the sign is fixed. Breach any one of those conditions and the deemed consent simply doesn’t apply, whether or not you realised it.
The thresholds that matter most in practice:
- Adverts over a small size threshold generally require express consent
- Illuminated signs usually need express consent regardless of size
- Temporary event notices are typically limited to a moderate size
Express consent applications in England cost £174 for business and advance directional signs, and £610 for other adverts, with decisions normally issued within 8 weeks of validation.
Deemed consent is a privilege, not a guaranteed right. Local authorities can restrict or withdraw it entirely in conservation areas, National Parks, or other areas of special control, so a sign that would be perfectly fine on a high street elsewhere might need full permission in a heritage town centre. Always check your council’s local policy statement before assuming the national default applies to your premises.
What do councils actually weigh up when deciding?
Local planning authorities are legally restricted to two considerations when assessing an advertisement application: amenity and public safety. Commercial need, however strong your business case, carries no legal weight in the decision.
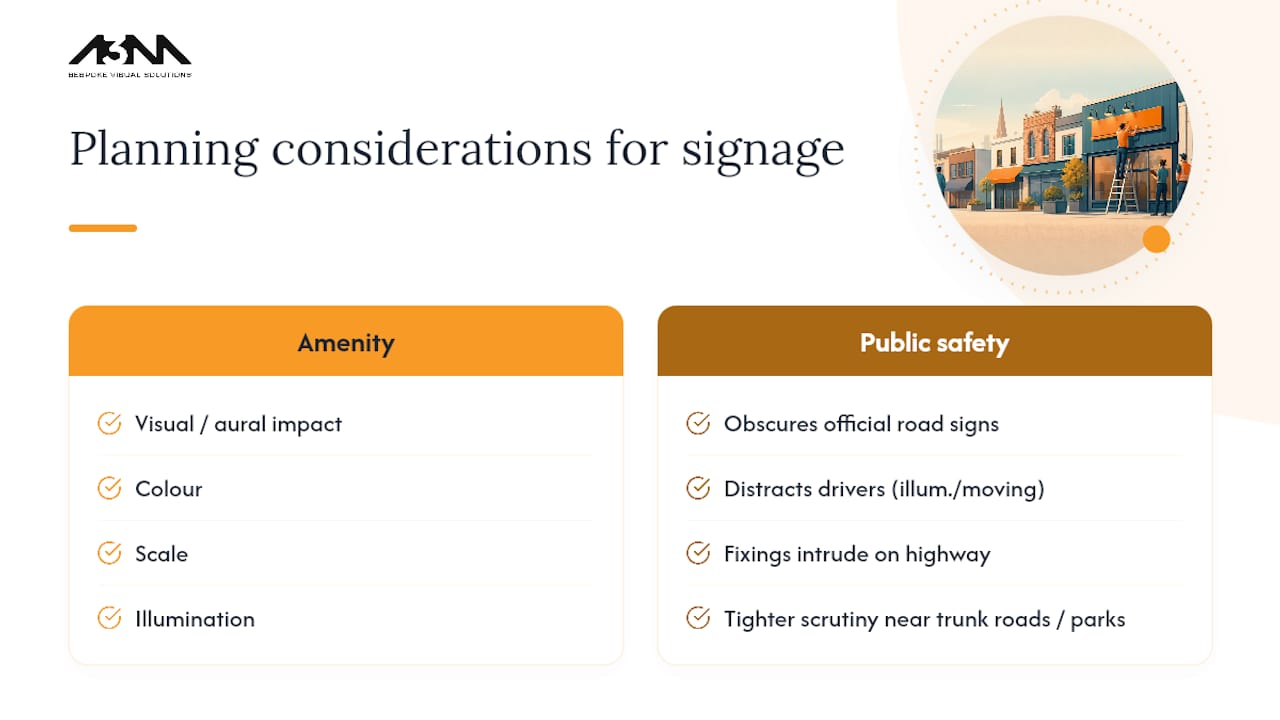
Amenity covers the visual and sometimes aural impact of a sign on its surroundings. A brash, oversized fascia sign on a listed Georgian building or in a designated conservation area is far more likely to be refused than the identical sign on a 1990s retail unit. Councils weigh colour, scale, illumination and materials against the character of the street.
Public safety is about whether the sign creates a hazard. Common objections include signs that obscure official road signs, illuminated or moving displays that distract drivers, or fixings that intrude onto a highway boundary. Signage near trunk roads, in National Parks, or within the Broads often faces tighter scrutiny for exactly this reason, and authorities can and do refuse consent purely on these grounds even when the design itself is inoffensive.
Your checklist for applying for advertisement consent
Get your paperwork right the first time and you cut weeks off the process. Councils reject or delay a striking number of applications simply because the submission is incomplete.
- Prepare a location plan showing the site in its wider context, plus a detailed site plan
- Draw scaled elevations of the proposed sign, including dimensions, materials and colours
- Specify illumination details if the sign lights up: type, brightness, hours of operation
- Confirm the proposed duration, particularly for hoardings or temporary event signage
- Secure written landowner permission before you submit, even if you’re the leaseholder
- Check highway authority involvement if the sign sits near a public road; local authorities hold powers under Section 132 of the Highways Act 1980 to remove unauthorised fixings on the highway
- Submit to the correct local planning authority, which under the 2007 Regulations must be the authority for the area where the advertisement will be displayed
Pro Tip: Book a pre-application chat with your local planning authority before you commission any artwork. Many councils will informally flag amenity concerns at this stage, saving you a redesign after a formal refusal.
If your premises is listed, or you’re working on a heritage high street, get a signage specialist involved early rather than after a refusal notice lands.
What happens if you get it wrong
Displaying an advertisement without the necessary consent is a criminal offence, not simply a civil planning matter. Local authorities can issue a discontinuance notice requiring removal of an existing sign even where it once had consent, if it’s now judged to cause harm to amenity or safety.
Where a sign is fixed unlawfully to a structure on the highway, the authority may remove it directly under the Highways Act, often at the owner’s cost. If you receive a notice, act quickly: gather your paperwork, establish whether retrospective consent is realistic, and consider whether relocating or resizing the sign resolves the objection faster than a formal appeal.
Refused applications carry a right of appeal to the Secretary of State, though this route typically takes months rather than weeks, so it’s rarely the fastest fix. Listed buildings add another layer of risk: even signage that would normally be exempt or deemed permitted needs separate listed building consent, and this is a frequent, expensive surprise for business owners who assumed the standard rules applied.
What A3m sees business owners get wrong on signage compliance
Most refusals we come across trace back to procurement shortcuts, not bad design. Before ordering, run a planning search, confirm landowner permission in writing, and prepare an installation method statement, particularly for anything fixed to a listed or historic building.
Design choices matter more than business owners assume:
- Sympathetic materials and finishes reduce amenity objections far more reliably than a smaller sign
- Proportionate lettering, scaled to the building rather than maximised for visibility, tends to sail through applications
- Low-level or timed illumination avoids the automatic scrutiny that full-brightness lighting attracts
- Discreet mounting details that don’t intrude onto a highway boundary avoid Section 132 disputes
Pro Tip: Ask any signage specialist you’re considering how many applications they’ve supported with your local authority specifically. Familiarity with a council’s particular sensitivities is worth more than generic planning knowledge. A3m’s work on compliant public sector signage reflects this same principle: design for the site’s constraints from the outset, not after a refusal.
The gap between planning theory and what actually gets refused
Most guidance treats advertisement consent as a binary compliance exercise: check the size, check the illumination, submit the form. That misses where the real risk sits. The two statutory tests, amenity and public safety, are judgement calls, and councils apply them with wildly different appetites depending on conservation status, local policy statements, and even which planning officer picks up the file.
Business owners who treat the 0.3 square metre threshold as the whole story get caught out precisely because deemed consent is conditional, not automatic. I’d argue the more useful mental model isn’t “is my sign under the size limit?” but “would this sign look at home on this specific street?” That’s a design question as much as a legal one, and it’s why the businesses that sail through applications tend to be the ones who involve someone with actual signage production experience before they draw up the artwork, not after a council objects to it.
The conventional advice to “check the Planning Portal and submit your form” is correct but incomplete. It skips the local policy statements that often matter more than the national default, and it under-weights how much a sympathetic material or fixing choice can neutralise an amenity objection before it’s even raised.
— Steve
Get your signage designed right the first time
Getting a planning application right the first time saves you weeks and the cost of a redesign after refusal. A3m works as the production partner that handles both sides of that problem: we design and manufacture signage built around your local authority’s amenity and safety concerns from the start, rather than leaving you to retrofit a rejected design.
Whether you need a fascia sign for a listed high street unit, hoardings for a development site, or a full wayfinding scheme across multiple premises, our signage service covers scaled drawings, material specification and illumination detail, the exact documentation your council will ask for. We also produce the technical drawings that support planning submissions; if your project needs bespoke fixtures alongside signage, our partner’s CAD drawing service is worth a look for accurate scaled plans. For construction and development sites, our guide to property development hoardings covers duration and application considerations specific to temporary signage.
Get in touch with A3m today for a quote on your signage project, and we’ll help you work out exactly what your local authority will need to see.
Sources
For the definitive rules, go straight to the Planning Portal’s adverts and signs guidance and Gov. The statutory text sits in the 2007 Regulations, with practical explanation in the outdoor advertisements booklet. Use your council’s website to find local policy statements before applying.
- Planning permission - Adverts and signs
- Outdoor advertisements and signs: a guide for advertisers
- The Town and Country Planning (Control of Advertisements) (England) Regulations 2007
- Do I need advertisement consent? — Planning House
Recommended
- Signage meaning: a clear UK guide – A3M
- Property development site signage: a 2026 compliance guide – A3M
- Hoarding signage in construction: the 2026 UK guide – A3M
- Sustainable signage materials benefits for UK businesses – A3M

Wall graphics cost UK: 2026 price guide for businesses
Printed vinyl wall graphics typically start from around £35 to £36 per panel supply-only, with installed costs pushing that higher once labour and access are factored in. Printed wallpaper is usually priced by the square metre, from about £17 per m², while repositionable fabric starts nearer £60 per panel. Cut vinyl lettering sits lower again for simple text-only jobs.
As a rule of thumb: a standard 3m × 2.5m office feature wall, fully installed, usually lands between £150 and £400 depending on material choice and wall condition. Before you ring round for quotes, have these ready:
- Exact wall measurements (width × height in metres)
- Photos of the wall, including any damage or texture
- Your preferred material or finish, if you already have one in mind
- A rough installation date and any access restrictions
Key Takeaways
Wall graphics pricing in the UK depends primarily on material choice, wall size, surface condition and installation complexity, with larger projects reducing the price per square metre.
| Point | Details |
|---|---|
| Material sets the baseline | Printed vinyl starts from around £35 to £36 per panel; wallpaper from about £17 per m²; fabric from roughly £60 per panel. |
| Feature walls follow a predictable band | A standard 3m × 2.5m office wall typically costs £150 to £400 installed depending on material. |
| Scale lowers unit cost | Banded rates for multi-site projects can fall from around £77/m² to £65/m² as project size increases. |
| Surface condition drives extra cost | Cracked, textured or previously papered walls need preparation that adds directly to labour time. |
| A3m offers a single-supplier route | In-house production, UK-wide installation and sustainable materials reduce coordination cost on larger rollouts. |
Table of Contents
- How much do wall graphics cost by material type?
- What makes one wall graphics quote higher than another?
- What would a typical wall graphics project actually cost?
- How do lead times and scheduling affect the price?
- How long do wall graphics last and what upkeep do they need?
- What should you send a supplier for an accurate quote?
- Why choose an established UK print partner for wall graphics?
- What are typical payment terms for wall graphics in the UK?
- Bespoke design versus ready-made graphics: what’s the price gap?
- Do special finishes like metallic or textured surfaces cost more?
- Are sustainable wall graphics materials more expensive?
- What other costs sit inside a wall graphics quote?
- Sources
How much do wall graphics cost by material type?
Material choice drives most of the price difference you’ll see between quotes, so it’s worth understanding what you’re actually paying for before you compare numbers.
Printed vinyl is the most common choice for office and retail feature walls. Standard calendared vinyl starts from around £35 to £36 per panel, while cast vinyl, which lies flatter and lasts longer, sits above that. Printed wallpaper is different: it’s sold by area rather than by panel, from about £17 per m², and works out more economical across large, continuous walls. Repositionable fabric costs more upfront, typically from £60 per panel, but it lifts cleanly off plaster without residue. Cut vinyl lettering (logos, wayfinding text, simple graphics without a background) is usually the cheapest option per job because there’s no full-bleed print involved.
Statistic Callout: Repositionable fabric commonly starts at roughly double the price of standard printed vinyl per panel, yet it removes the redecoration and patch-repair costs landlords often charge at lease end.
A few finish choices shift the price further:
- Laminate overlaminate for high-traffic corridors and washrooms
- Matt versus gloss finish, mostly an aesthetic choice with minimal cost difference
- PVC-free or Class O fire-rated substrates for public buildings and escape routes
- Textured or fabric-backed options for boardrooms and hospitality spaces
One thing that rarely changes the print cost: how complicated your image is; for examples of impactful visual campaigns that drive results, see these outdoor brand campaign examples that drive real results. A detailed photograph prints for the same price as a flat colour block. What does add cost is extra finishing, colour proofing, or splitting a complex image cleanly across panel joins.
What makes one wall graphics quote higher than another?
Two quotes for what looks like the same wall can differ by hundreds of pounds, and it’s rarely down to one supplier “overcharging”. A handful of practical factors explain most of the gap.
- Size and pricing method. Square metre pricing generally drops as the area increases, because setup and material waste get spread across more coverage. A single small panel costs more per m² than a full corridor run.
- Installation complexity. Working at height, needing scaffold towers or podium steps, or fitting outside normal hours all add labour time and, therefore, cost.
- Surface condition. Cracked plaster, old wallpaper, uneven filler or flaking paint all need addressing first. 3M’s own application guidance is explicit that substrate condition materially affects installation time, and by extension, price.
- Artwork readiness. Files that need vector conversion, pattern matching across panel joins, or a proof round before print all carry a design or prep fee.
Pro Tip: Ask your supplier for a wall inspection or photos-based assessment before you commit to a quote. Surface prep is the single most common reason installed prices exceed the “from” figure you saw online.
What would a typical wall graphics project actually cost?
Numbers mean more with a worked example attached, so here are three common UK scenarios with their assumptions stated plainly.
- Example A: small office feature wall, 3m × 2.5m (7.5m²). Assuming a standard painted wall, normal daytime access and no scaffold: printed vinyl typically runs £150 to £280 installed; printed wallpaper, calculated at roughly £17 per m² plus fitting, often costs similarly; repositionable fabric runs higher, often in the few hundreds of pounds range given its higher per-panel starting cost; a cut vinyl logo alone (no full-bleed background) can come in under £150.
- Example B: 10m corridor, 2.5m high (25m²). Here the per-m² maths starts working in your favour. Wallpaper priced by area benefits most from the larger run, while panel-based vinyl also sees a lower blended rate once setup costs are spread across more panels.
- Example C: multi-site or school rollout. Suppliers serving institutional clients often publish banded rates that fall as total project value rises. One UK specialist’s published bands run from around £77/m² for small single-site jobs down to roughly £65/m² once a project scales up across several locations.
Statistic Callout: That £77/m² to £65/m² banded range shows how ordering across multiple sites or classrooms in one contract, rather than piecemeal, can meaningfully lower your average unit cost.
How do lead times and scheduling affect the price?
Production time varies by material, and rushing it usually costs you.
- Standard printed vinyl and cut lettering typically need a shorter turnaround than printed wallpaper, which involves more careful colour matching and panel sequencing.
- Express or rush production is available from most UK suppliers but usually carries a percentage uplift on the standard price.
- Booking installation during school holidays or a retailer’s quiet trading period often avoids disruption charges, and sometimes reduces the need for after-hours labour altogether.
- Evening, weekend or overnight installs, common in retail and hospitality where the space can’t close, add to the day rate because of overtime and reduced working windows.
How long do wall graphics last and what upkeep do they need?
Lifespan depends heavily on the material and where it’s fitted, so budgeting for a five-year refresh looks very different from budgeting for fifteen.
- Standard printed vinyl typically lasts 5 to 10 years depending on light exposure, footfall and whether it’s laminated.
- Repositionable fabric tends to run 3 to 5 years in heavy-use areas, trading longevity for the ability to remove it without damaging the wall.
- Printed wallpaper can last 7 to 15 years when the substrate is prepared properly and adhesion is done correctly, per 3M’s application guidance.
Direct sunlight, damp and abrasive cleaning all shorten lifespan across every material.
Pro Tip: If you’re in a leased office or retail unit, repositionable fabric is usually the more cost-effective choice overall. It avoids the wall repair and repainting charges landlords often deduct from a deposit when standard vinyl comes down.
What should you send a supplier for an accurate quote?
Getting a like-for-like comparison between suppliers means giving them all the same information up front.
- Measurements and photos. Provide width × height for every wall, plus clear photos showing the surface, corners and any visible damage.
- Wall finish and condition. Note whether it’s painted plaster, textured, previously wallpapered, or has any known defects.
- Access and timing. State your preferred installation date, working hours available, and whether the space needs to stay open during fitting.
- Artwork status. Say whether you’re supplying finished, print-ready files or need design and repro work, since this changes the quote significantly.
- Direct questions to ask. Confirm whether the quote includes installation, removal of old material, a warranty period, fire-rated substrate options, a test patch, and appropriate insurance and COSHH compliance for the installers.
Why choose an established UK print partner for wall graphics?
A3m manufactures large-format print in-house, covering wall and window graphics, branded environments, exhibitions and signage for UK businesses. For multi-site rollouts or jobs needing complex finishes, working with one experienced partner across every location usually reduces total project cost and risk compared with managing several local suppliers separately.
- In-house production for print, signage and branded environments
- Site survey and installation available across the UK
- Suited to multi-site retail, hospitality and education rollouts
What are typical payment terms for wall graphics in the UK?
Most UK print suppliers, including those handling wall graphics, work on a deposit-plus-balance structure rather than full payment upfront or full credit.
For new commercial clients, expect to pay the deposit before artwork proofing or production begins. This protects the supplier against bespoke material costs on a cancelled job and, in practice, speeds up your own turnaround, since production rarely starts until funds have cleared. Established business relationships and multi-site framework agreements sometimes move to monthly invoicing with 30-day terms, but this is usually only offered once a track record exists between the two parties.
Larger institutional projects, such as school or council rollouts spanning several sites, often use staged payments tied to delivery milestones: a deposit to commence, a payment on proofing sign-off, and a final balance on completed installation. This spreads cashflow risk for both sides and gives you natural checkpoints to review artwork before the whole job is committed to print.
Whatever the structure, get payment terms confirmed in writing alongside the quote itself, not left to a verbal agreement. A written schedule should state what triggers each payment, whether VAT is included in the figures quoted, and what happens if installation is delayed on your side, for instance if a site isn’t ready on the agreed date. Ambiguity here is one of the more common sources of dispute on larger contracts.
Bespoke design versus ready-made graphics: what’s the price gap?
Ready-made or template graphics are, unsurprisingly, the cheaper route when you need something generic and don’t have brand-specific requirements. A stock nature scene, an abstract pattern, or a pre-designed motivational typography piece can be printed and fitted without any design time built into the price, since the artwork already exists in print-ready form.
Bespoke design work changes the cost picture in one specific way: it adds a design or artwork fee on top of the print and installation cost, rather than making the print itself more expensive. That fee typically covers concept development, brand colour matching, file preparation for large-format output, and at least one round of proofing. For a business wanting its exact brand palette, logo integration, or a custom illustration reflecting a specific space, this is usually the only realistic option, since a template can rarely match a brand guideline precisely.
The gap narrows considerably if you already have finished, print-ready artwork from an in-house designer or agency. In that case, a “bespoke” job costs close to the same as a template one, because the supplier’s job is simply reproduction and fitting rather than creation. The false economy to watch for is choosing a template because it looks cheaper, then paying for revisions to make it fit your brand anyway, at which point you’ve paid twice: once for the template licence, once for the changes.
For most commercial clients, particularly in hospitality and retail where brand consistency matters, the bespoke route pays for itself through a result that actually matches the rest of the space. A3m’s guide to large-format print covers the production side of this in more detail.
Do special finishes like metallic or textured surfaces cost more?
Yes, and the increase is usually proportional to how much the finish changes the standard production process. A flat matt or gloss laminate over standard printed vinyl adds a modest amount to the base panel price and is one of the most common upgrades for high-traffic corridors, since it protects the print from scuffing and light abrasion.
Metallic and textured finishes cost more because they typically require a different substrate entirely, not just a different coating. Textured wallcoverings that mimic fabric, brushed metal or concrete need specialist material stock, which costs more to buy in and is often only available from a narrower range of manufacturers. Metallic finishes, whether a foil-effect laminate or a genuine metallic substrate, add cost partly for the material and partly because colour proofing against a reflective surface takes more care to get right.
Class O fire-rated finishes, required in many public buildings, schools and escape routes, sit in a similar bracket: not dramatically more expensive per m², but noticeably above standard PVC vinyl, and worth confirming early if your building falls under stricter fire regulations. The practical advice here is to specify any required finish before you request quotes, rather than after, since switching substrate midway through a project often means re-quoting the whole job rather than a simple add-on.
Complex multi-panel designs that need precise pattern matching across joins also add cost, not because the print itself is harder, but because installation takes longer and mistakes are less forgiving.
Are sustainable wall graphics materials more expensive?
Sustainable material options have narrowed the price gap with standard substrates considerably, and for many jobs there’s now little practical difference. PVC-free vinyl alternatives, recyclable wallpaper stocks and water-based ink printing are increasingly offered as standard by UK large-format suppliers rather than as a premium add-on.
Where a genuine cost difference remains, it tends to sit with specialist substrates: fully recyclable or biodegradable wallcoverings, and materials certified to specific environmental standards for public sector procurement, can carry a modest premium over standard PVC vinyl. This is usually a material cost difference rather than an installation one, since fitting time is broadly comparable across most substrates.
For organisations with sustainability commitments, particularly local authorities, education clients and hospitality brands with environmental policies, the more relevant cost consideration is often longevity rather than the sticker price. A durable, well-fitted sustainable wallpaper that lasts 10 to 15 years works out cheaper over its lifetime than repeatedly replacing a shorter-lived budget option. A3m’s sustainable print solutions are built around this kind of lifecycle thinking rather than treating eco materials as a separate, pricier tier.
What other costs sit inside a wall graphics quote?
A headline “per panel” or “per m²” figure rarely captures every cost in a real project, and unbundling the components helps you spot where quotes genuinely differ.
Design fees cover concept work, brand-colour matching and layout for bespoke jobs, typically charged as a separate line rather than folded into the print price. Artwork creation or licensing applies if you need original illustration work, or if you’re licensing stock photography or an artist’s design for reproduction. Some suppliers include a set number of proof rounds within the design fee; further changes are usually billed separately.
Installation covers labour, access equipment and any specialist tools needed for the substrate. Removal of old graphics, often overlooked until a refit is booked, can add a meaningful sum if the previous material was poorly applied or has been up for years, since stripping degraded vinyl or adhesive residue takes longer than fitting new material. Warranty and after-care, such as a call-out to fix a lifting edge, is sometimes included for a defined period and chargeable afterwards.
Getting a single quote that itemises each of these, rather than one bundled figure, makes it far easier to compare suppliers fairly and to spot which one has quietly left something out.
Common pitfalls that push wall graphics budgets over
Scope creep is the biggest budget-wrecker: adding an extra wall, upgrading to a laminate finish, or discovering damp behind old wallpaper after the job’s already been priced. Wallpaper suits large continuous runs; fabric suits leased spaces you’ll need to reinstate. Bring your supplier in early, before the budget is fixed, not after.
— Steve
Get a bespoke wall graphics quote from A3m
A3m runs its own in-house production, meaning your wall graphics come from a single UK team rather than a chain of subcontractors, which is usually the fastest route to a firm price and a firm date. That matters most when you’re comparing quotes and finding the numbers vague: A3m offers a site survey, full UK installation, and sustainable material options as standard, so what you’re quoted is what you actually pay.
To get a quick, accurate quote, send over your wall measurements, a couple of photos of the surface, your preferred material if you have one, and your target installation date. If you want to see finishes and past projects before deciding, the A3m gallery is worth a look, and the large-format print manufacturing overview explains the in-house capability behind every quote. Get in touch with your details and A3m will come back with a clear, itemised price.
Sources
- Printed Wall Graphics | UK Custom Office Wall Graphics & More | UK Sign Shop
- School wall graphics costs in the UK for 2026 | Cubed Creative
- 3M application guidelines: applying graphics to walls
Recommended
- Luxury retail window graphics explained: 2026 UK guide – A3M
- Service Graphics alternatives for UK marketing teams – A3M
- Vinyl Decals vs. Full Wraps: The Ultimate 2026 Comparison for UK Businesses – A3M
- Types of window graphics retail: your 2026 guide – A3M

Sign fixing methods: a professional's guide to secure installation
Mechanical anchors and studs are the default choice for permanent external signage, offering the load capacity and weather resistance that fascias and masonry demand. For premium dimensional lettering, locators and standoffs deliver a cleaner finish; for smooth, sheltered panels, VHB and structural adhesives can work well, provided the substrate is right. Cable ties and banding suit mesh fencing and temporary events, while magnets belong strictly to short-term steel applications.
- Permanent external signs: mechanical anchors or through-bolts into masonry or steel
- Premium letters and logos: locators or standoffs with concealed fixings
- Smooth, sheltered panels: VHB tape, often backed up mechanically
- Temporary fencing or events: UV-rated cable ties or clip fittings
- Short-term steel-only fixes: magnets, never for wind-exposed or long-term use
Pro Tip: Combine adhesive and mechanical fixings on any critical external panel where a visible screw head is unwelcome. It’s the belt-and-braces approach most experienced installers default to, and SafetySignHub’s installation guidance backs it for good reason. Anything projecting or carrying real wind load should go through documented pull testing before it goes anywhere near a wall.
Key Takeaways
The right sign fixing method depends on load, substrate and permanence, and mechanical anchors remain the safest default for permanent external signage.
| Point | Details |
|---|---|
| Match method to substrate | Masonry, steel and cladding each demand different anchor types and embedment depths. |
| Use stainless outdoors | SS304 or SS316 fasteners resist corrosion far better than zinc-plated alternatives. |
| Pull test high-load signs | Projecting or heavy signs need documented pull testing, not just a visual check. |
| Inspect on a schedule | Annual checks, biannual in coastal or high-wind sites, catch failures before they escalate. |
| A3m manages the whole job | A3m specifies, manufactures and installs signage with fixing methods engineered in from the survey stage. |
Table of Contents
- Sign fixing methods at a glance: which family fits your job?
- Mechanical fastenings: screws, anchors, studs and plugs
- Locators and standoffs for dimensional lettering
- Rails, trays and bracket systems for heavy signs
- When do adhesive fixings and VHB tape actually work?
- Temporary and specialist fixings: cable ties, banding and magnets
- How do you choose the right fixing method for your project?
- What UK standards and competence checks should you insist on?
- Maintenance and inspection schedule for fixed signage
- What installers get wrong most often
- Get your signage specified and installed properly
- Sources
Sign fixing methods at a glance: which family fits your job?
Every fixing decision comes down to five questions: how much does the sign weigh, is it permanent or temporary, does it need to look invisible, what’s the substrate, and how exposed is the site to wind and salt air? Answer those first, and the right method usually becomes obvious.
- Mechanical fixings (screws, anchors, studs): permanent, high-load, most substrates
- Locators and standoffs: premium visual finish, moderate load, needs flat substrate
- Rails and trays: heavy or serviceable signs, distributes load across structure
- Adhesives and VHB tape: light panels, smooth non-porous surfaces only
- Cable ties, clips, magnets: temporary or low-risk applications
Coastal sites push everything towards stainless steel. Listed buildings and cladding warranties often rule out drilling altogether, and high wind exposure turns a “nice to have” pull test into a requirement.
Mechanical fastenings: screws, anchors, studs and plugs
For solid masonry, rawl plugs handle light to moderate loads; chemical anchors suit denser concrete or where vibration resistance matters; through-bolts are the answer for steel structures or where you need certifiable load ratings. Embedment depth has to match the manufacturer’s data for that specific substrate, not a rule of thumb.
- Match anchor type to substrate density and sign weight, not just hole size
- Specify SS304 or SS316 stainless for anything outdoors, never zinc-plated
- Use fixing templates for consistent spacing across multi-point installations
- Torque to the fastener manufacturer’s spec, and pull test projecting or high-load signs
Pro Tip: Zinc-plated screws look fine on day one and rust-streak your fascia within a year. It’s one of the most common causes of callback work in the trade, and switching to stainless fasteners costs almost nothing extra at spec stage.
Locators and standoffs for dimensional lettering
Snap locators and brass or nickel locator systems let dimensional letters sit flush against a fascia without visible screw heads, which is why premium retail and hospitality signage leans on them so heavily. Standoffs pull letters or panels forward from the wall instead, creating a shadow gap that reads well from a distance.
- Choose standoff length based on desired shadow depth and thermal movement allowance
- Use concealed fixings behind the letter face where the brief calls for a seamless look
- Fit second-generation acrylic locking nuts rather than standard nuts for outdoor letters
- Check vibration resistance where signs sit near traffic, extraction units or high footfall
Thermal expansion matters more than most specifiers expect. Aluminium letters move noticeably across a UK seasonal temperature range, so standoffs need enough tolerance to avoid stress cracking at the fixing point.
Rails, trays and bracket systems for heavy signs
Rails and trays exist to spread load across a wall’s structural backing rather than concentrating it on a handful of screw points, which is exactly why they’re the right call for heavy fascia signs, illuminated boxes or anything that needs periodic servicing.
- Fix rails into structural steel or masonry, never into cladding or render alone
- Space bracket points evenly and check level before final fixing, not after
- Route cables and drainage carefully on illuminated trays to prevent water ingress
- Favour trays or upstands on listed buildings, where drilling into original fabric is restricted
A tray system also speeds up future maintenance considerably, as explained in this digital signage design guide. Swapping out an illuminated panel takes minutes when it lifts off a rail, compared with a full re-drill if it was fixed directly. Our architectural signage guide covers how this plays out on real fascia projects.
When do adhesive fixings and VHB tape actually work?
VHB tape and structural adhesives work well on smooth, clean, non-porous surfaces carrying light loads, sheltered from direct wind pressure. On brick, render or anything textured, adhesion drops off fast, which is why SafetySignHub’s guidance is blunt about matching the method to the surface, not the sign.
- Prime the substrate where the manufacturer specifies it, and respect application temperature windows
- Stick to the tape’s rated weight limit, and back it up mechanically for anything critical
- Expect bond strength to degrade slowly with UV exposure, moisture cycling and thermal movement
Pro Tip: Never rely on adhesive alone above head height outdoors. A mechanical fixing hidden behind the panel edge gives you the clean look and the safety margin.
Temporary and specialist fixings: cable ties, banding and magnets
Temporary doesn’t mean careless. Cable ties on mesh or fencing need to be UV-rated, used in multiples per sign, and checked regularly, since a single tie fatigues faster than most people expect.
- Fit at least four UV-stabilised cable ties per sign panel on mesh or fencing
- Use clip fittings or screw banding for post-mounted road and directional signs
- Reserve magnets strictly for temporary fixes to flat steel, indoors or sheltered
- Inspect temporary fixings weekly in exposed locations, more often after storms
- Never treat a temporary method as a long-term or high-wind solution
Post-mounted signage has its own conventions worth following, and Road-signs sets out the clip and banding approach used across most UK post installations.
How do you choose the right fixing method for your project?
Work through this in order, and you’ll rarely end up specifying the wrong method.
- Measure load and wind exposure — weight, sail area, and site wind zone dictate everything downstream
- Identify the substrate — masonry, steel, cladding or render all demand different anchor types
- Decide permanence and visibility — permanent, removable, or temporary, and whether fixings must be concealed
- Specify corrosion resistance — SS304 or SS316 for coastal or long-term exposure, per 8 Shop Signs’ fastener guide
- Confirm installer competency — CSCS, PASMA or IPAF for access work, and documented anchor training
Pro Tip: Ask any installer for their last pull-test certificate before they go near your fascia. If they can’t produce one, that’s your answer.
Projecting signs, illuminated units and anything over a certain weight threshold should always trigger pull testing and, where load is significant, engineer sign-off. Keep survey notes, substrate photos and fixing schedules on file. It’s the paperwork that protects you when a warranty dispute or insurance claim lands three years down the line.
What UK standards and competence checks should you insist on?
Fixing decisions sit at the intersection of two British Standards that most sign buyers never hear about until something goes wrong. BS 8539 governs anchor selection and installation into concrete and masonry, while BS 7671 covers the electrical safety of illuminated signage. The BSGA Knowledge Hub treats fixing specification as a safety issue, not a finishing detail, and recommends coordinating with the host substrate before manufacture even begins.
- Require documented pull testing on any projecting or high-load sign
- Confirm installer CSCS cards and PASMA or IPAF certification for access equipment
- Ask for anchor-specific installation training records, not just general trade experience
- Retain test certificates and installation photographs for the life of the sign
Visual inspection alone cannot confirm anchor performance. Pull testing verifies what the eye can’t, and the BSGA’s practical guidance treats it as standard practice on projecting or high-load installations, not an optional extra.
Installer refresher training every five years, covering anchor systems and access equipment, is the benchmark worth procuring against.
Maintenance and inspection schedule for fixed signage
A sign that’s been up for two years needs the same scrutiny as one going up tomorrow.
- Annually, check fixing torque, look for rust streaks or displacement, and inspect seals on illuminated boxes
- Biannually in coastal or high-wind sites, given faster corrosion cycles
- Escalate to pull testing if you see movement, cracking around fixing points, or unexplained gaps
- Replace, don’t patch, once corrosion has taken hold in a structural fixing
- Log every inspection, since gaps in the record undermine warranty and liability claims later
Our guide to outdoor weatherproof signage goes into more depth on how UK weather cycles accelerate wear on external fixings.
What installers get wrong most often
The recurring mistake isn’t the fixing choice, it’s skipping the substrate survey because the schedule’s tight. Drill first, discover cavity insulation or a rendered lightweight block second, and you’ve created a callback. A3m’s process builds substrate checks into the manufacturing brief before a single bracket gets cut, which is the cheapest insurance on a large rollout.
Get your signage specified and installed properly
There are plenty of ways to source signage fixings, from local fabricators to national installer networks, but few combine specification advice with in-house manufacture and managed installation under one roof. A3m does. Our production teams build every sign with the correct fixing method engineered in from the start, and our installers carry the CSCS, PASMA and IPAF competency the standards call for.
Whether you’re rolling out fascia signage across twenty sites or specifying a single illuminated panel, A3m can survey the substrate, recommend the right fixing family, and manufacture to fit before installation day arrives. Get in touch to request a site survey or a quote through our signage services page, and we’ll talk you through pull testing options for anything projecting or high-load.
Sources
- KH-MECHANICAL-FIXING.pdf
- Safety Sign Fixing Methods: Screws, Adhesive, Magnets and Cable Ties | SafetySignHub
- Fastener Guide for Sign Makers | 8 Shop Signs
Recommended
- Property development site signage: a 2026 compliance guide – A3M
- Event management signage workflow: a practical guide – A3M
- Wayfinding signage design: a practical UK guide – A3M
- Indoor directional signage: a guide for facility managers – A3M

Site safety boards UK: what your site entrance needs
For most UK construction sites, the right choice is a multi-message board at the entrance, produced to ISO 7010 symbol standards, showing your site ID, principal contractor details, emergency contacts and PPE rules. Before you order anything, check one thing first: does the supplier design to ISO 7010, and can they prove readability at your actual viewing distance?
- A multi-message site safety board suits most entrances, not a scatter of separate small signs.
- Confirm ISO 7010 symbols, plus site ID, emergency contact and PPE information, sit on the same panel.
- Ask for a readable-size proof and ask what materials they’d recommend for your project length.
Key Takeaways
A compliant site safety board pairs ISO 7010 symbol accuracy with the legal permanence and maintenance duties set out in the 1996 Regulations, and gets audited on a schedule, not just at installation.
| Point | Details |
|---|---|
| Start with the legal check | Confirm significant risks remain after other controls before assuming a sign is even required. |
| Match material to project length | Use Correx for short jobs, rigid PVC for medium-term, aluminium composite for long or exposed sites. |
| Keep the reading order simple | Site ID and reporting instructions first, PPE and emergency details second, to avoid overcrowding. |
| Build in a maintenance owner | Name one person responsible for checking and updating the board, not just installing it. |
| Choose a manufacturer for speed | A3m’s in-house production and web-to-print options cut turnaround on updates and repeat orders. |
Table of Contents
- What the Health and Safety (Safety Signs and Signals) Regulations 1996 require
- What should a site safety board include? A concise checklist
- Materials, size and legibility: pick a board that lasts
- Standard kits vs bespoke boards: which do you need?
- Supplier checklist: questions to ask before you order
- How in-house manufacturing simplifies compliance and reordering
- Why compliance guides miss the maintenance problem
- Get a sample, quote and proof for your site safety board
- Primary guidance to consult
- Sources
What the Health and Safety (Safety Signs and Signals) Regulations 1996 require
The legal starting point is simple. Employers must provide safety signs wherever a risk assessment shows significant risks remain after other controls are in place, and where a sign will genuinely reduce that risk further. If your site has moving plant, work at height, or restricted zones, a sign isn’t optional decoration. It’s a control measure.
The Health and Safety (Safety Signs and Signals) Regulations 1996 set out the actual mechanics: shape, colour, and when a signboard must be permanent rather than temporary. Prohibition signs, warnings, and emergency route markers all fall under this permanence requirement, which rules out a laminated sheet cable-tied to a fence post and left to fade over a winter.
HSE guidance adds a duty that catches a lot of site managers out: signs must be maintained, and anything unfamiliar must be explained to workers, not just displayed and forgotten.
One figure worth remembering: HSE’s L64 guidance on the 1996 Regulations references BS/ISO standards for symbol sizing and placement, meaning “readable” isn’t a subjective judgement. It’s a calculable spec based on how far away someone stands when they read it.
Three practical takeaways follow from this:
- Location matters as much as content. A board tucked behind a skip fails the regulation in practice, even if the wording is perfect.
- Illumination matters where a site runs shifts into darker hours or winter afternoons.
- Maintenance isn’t a one-off. Faded, cracked or peeling boards are treated as non-compliant, not just untidy.
What should a site safety board include? A concise checklist
Before you order a board, or audit the one already at your gate, run through this list. Practitioner guidance consistently recommends a clear reading order: identification and reporting instructions first, hazard and emergency information second. Overcrowding a single panel with every possible message actually reduces its compliance value, because nobody reads a wall of text at the gate.
- Site name and address, clearly visible from the road or approach.
- Principal contractor name and contact numbers, including an out-of-hours line if the site runs shifts.
- PPE requirements, shown using correct ISO 7010 pictograms rather than text alone.
- Prohibition messages (no unauthorised access, no naked flames, and similar) in the standard red circle format.
- Emergency assembly point location, with a simple arrow or map reference.
- First aider name and emergency contact numbers, updated whenever personnel change.
- F10 notification reference and CDM lead details, where the project is notifiable under CDM 2015.
- Date of last review and the person responsible for updates, so anyone checking knows the board isn’t stale.
Materials, size and legibility: pick a board that lasts
Material choice depends almost entirely on how long the board needs to survive outdoors, and UK weather is not gentle on cheap substrates. Three options cover most projects:
- Correx (corrugated plastic): cheap and light, fine for short-term works of a few weeks, but it flexes and fades quickly in UV.
- Rigid PVC (often called Foamex): a solid middle ground for medium-term sites, holding colour and shape well for several months.
- Aluminium composite (dibond): the choice for long-term or high-exposure installations, resisting warping, UV bleaching and impact far better than plastics.
Matching material to project length isn’t just a durability question, it’s a cost one. Paying for aluminium composite on a two-week job is wasted spend; using Correx on an eighteen-month build means replacing a peeling, unreadable board halfway through.
On sizing, the standard rule of thumb ties symbol and text height to viewing distance, so a board read from a car window at a site entrance needs noticeably larger lettering than one mounted beside a doorway. Mount at eye level where possible, avoid glare from reflective laminates facing direct sun, and check fixings are rated for wind loading if the board sits on open hoarding.
Pro Tip: *Ask your supplier for a digital proof scaled to the actual viewing distance, not a small preview on a laptop screen.
Standard kits vs bespoke boards: which do you need?
Most routine sites are well served by a standard multi-message kit. These come pre-designed with the common prohibition, mandatory and warning symbols already laid out, and they’re fast to order and inexpensive, which suits smaller contractors or short programmes where a fully custom layout isn’t worth the lead time.
Bespoke boards earn their higher cost when a site has unusual hazards, multiple phased stages, or when branding needs to appear alongside compliance information, something increasingly common on developer-led schemes where the hoarding also does marketing work.
A few procurement points worth settling before you commit:
- Send vector artwork for logos rather than low-resolution images, or expect a proofing delay while it gets recreated.
- Ask for a sample panel if you’re ordering across multiple sites, so colour and finish stay consistent between locations.
- Order a spare panel or two, particularly for information that changes often, like the named first aider or emergency contact.
- Consider modular insert systems if contact details or phase information shift regularly, so you’re not reprinting the whole board each time.
Supplier checklist: questions to ask before you order
A good supplier answers these without hesitation. A weak one gets vague fast.
- Do you design to ISO 7010 symbol standards, and can you show a sample? If they can’t answer this directly, move on.
- What materials do you recommend for a project of my length, and why? The answer should reference exposure and durability, not just price.
- Can I see a digital proof sized to my actual viewing distance? This catches legibility failures before they’re printed and shipped.
- What’s your turnaround for updates? Contact numbers and named personnel change; a board that takes three weeks to amend isn’t fit for a live site.
- Do you offer sample panels before a full order? Especially relevant for multi-site or repeat procurement.
Red flags are just as telling: a supplier who can’t name a standard they work to, has no samples to show, or quotes an unrealistically short lead time on a bespoke design, is worth questioning before you commit budget.
Pro Tip: Request a small trial order, one board, properly proofed, before committing to a batch across five or ten sites. It costs little and catches problems a screen proof never will.
How in-house manufacturing simplifies compliance and reordering
Working with a UK manufacturer that prints in-house, rather than outsourcing production, cuts the number of steps between your proof approval and a board arriving on site. A3m produces large-format signage using in-house facilities, which means fewer handoffs and faster turnaround when a contact number changes or a board needs replacing after storm damage.
For businesses running multiple sites, a web-to-print portal keeps layouts consistent across locations while still allowing local details, like site address or named first aider, to update independently. Durable, sustainable material options also reduce how often boards need replacing over a project’s life, which matters more on longer builds than the upfront unit price does.
Why compliance guides miss the maintenance problem
Most advice on this topic stops at the point of purchase. Get the right symbols, get the right size, get it installed, job done.
HSE’s own guidance is explicit that signs must be kept in good condition and understood by the workforce, yet almost nobody budgets time or money for checking a board after it’s gone up. A board that was perfectly compliant on installation day, with the wrong first aider’s name still listed four months later, is not a minor administrative slip. It’s a live compliance gap.
My honest view: spend less energy agonising over which shade of aluminium composite to choose, and more on deciding, in writing, who checks the board monthly and who owns the update process when contact details change. The correct pictograms matter, but an outdated board with perfect symbols still fails the workforce it’s meant to protect.
Get a sample, quote and proof for your site safety board
A3m is the practical alternative to juggling a generic sign catalogue and a separate print supplier for anything bespoke. Because production happens in-house, from proofing through to the finished panel, you get one point of contact, consistent finishes across every site in your portfolio, and a much faster turn on urgent changes, like a new emergency contact or a revised assembly point, without waiting weeks for a reprint.
Every board is produced with correct ISO 7010 symbol placement and can include the CDM-relevant details your notifiable project needs, from principal contractor information to the F10 reference. Material options range from short-term boards for a few weeks on site through to weather-resistant panels built for multi-year programmes, so you’re not overpaying for durability you don’t need or underspending on a board that won’t survive the winter.
Get in touch through A3m’s signage services page to request a sample panel or a quote, and ask for a proof scaled to your actual entrance viewing distance before anything goes to print.
Primary guidance to consult
Bookmark the 1996 Regulations and HSE’s safety signs guidance for the legal baseline, and the L64 booklet for practical sizing and placement detail. Supplier guides like The Safety Sheep Store’s content checklist are useful for layout, but always check them against HSE’s own position first.
Sources
- The Health and Safety (Safety Signs and Signals) Regulations 1996
- Safety signs - HSE
- Site Safety Boards UK: What to Include – The Safety Sheep Store
Recommended
- Hoarding signage in construction: the 2026 UK guide – A3M
- Wayfinding signage design: a practical UK guide – A3M
- Grand opening signage setup: your 2026 UK guide – A3M
- Signage meaning: a clear UK guide – A3M

Packaging board types: a specifier's guide to grades and uses
Six board families cover almost every packaging brief you’ll receive: solid bleached sulfate (SBS), folding boxboard (FBB), coated recycled board (CRB) or white-lined chipboard (WLC), coated unbleached kraft (CUK), greyboard/chipboard, and corrugated. Each one solves a different problem, and choosing the wrong family is the single most common cause of packaging rework we observe.
Paperboard itself is defined by caliper and multi-ply construction, which is what separates it from ordinary printing paper and from corrugated board’s fluted core. Here’s the shortlist by application:
- Cosmetics and premium retail — SBS, for the whitest base and cleanest foil/emboss results
- Everyday folding cartons (cereal, FMCG) — FBB, for the best stiffness-to-weight ratio
- Recycled-content claims — CRB/WLC, where sustainability messaging outweighs top-end print fidelity
- Craft, food-service or rustic branding — CUK/natural kraft, valued for its unbleached, fibrous look
- Rigid boxes and inner supports — greyboard/chipboard, chosen purely for bulk and structural stiffness
- Transit and e-commerce shipping — corrugated, for cushioning and stacking strength
Key Takeaways
Board selection works best as a chain decision: fibre and ply determine print fidelity, print fidelity determines finish options, and finish options determine converting cost and lead time.
| Point | Details |
|---|---|
| Match grade to function | Use SBS for premium print, FBB for everyday cartons, CRB/WLC for recycled claims, greyboard for rigid cores. |
| Specify caliper, not just GSM | Caliper drives fold and stiffness performance; always request both figures with tolerance ranges. |
| Request certificates, not labels | Ask for FSC/PEFC chain-of-custody documents and stated recycled-content percentages on invoices. |
| Proof on the real substrate | Foil adhesion and colour shift between stocks, so approve proofs on the nominated board and finish. |
| Bring in a manufacturing partner early | A3M offers in-house sampling, litho-lamination, and finishing to validate specification before a full production run. |
Table of Contents
- What are the main packaging board types?
- What technical specs actually define a board grade?
- How do you choose the right packaging board?
- Which finishes suit which board type?
- How sustainable are different packaging boards?
- What are typical GSM and caliper ranges by board type?
- What converting constraints affect board choice?
- When should you bring in a packaging or print partner?
- A manufacturer’s note on getting the spec right
- How A3M supports packaging board selection and production
- Sources
What are the main packaging board types?
Every commercial paperboard grade is a variation on the same theme: layered wood fibre, pressed and dried to a specified caliper, then coated or left natural depending on what the brand needs it to do on shelf. The differences between grades come down to fibre source, bleaching, ply count, and coating weight, and those variables decide everything from foil adhesion to recyclability. Trade guidance on board grades consistently groups the commercial market into the same handful of categories, which makes cross-supplier comparison reasonably straightforward once you know what to ask for.
SBS (solid bleached sulfate)
Made from bleached virgin softwood fibre, SBS gives you the brightest, most consistent print surface on the market. It takes foil, embossing, and fine screen printing better than any other grade, which is why cosmetics, pharmaceuticals, and premium spirits packaging default to it. Food-contact grades are widely available, and the surface holds tight registration on multicolour litho work.
FBB (folding boxboard)
FBB uses a bleached or unbleached chemical pulp outer layer over a mechanical pulp core, giving it excellent stiffness for its weight. It’s the workhorse of European folding carton production. Cereal boxes, confectionery, and toiletries packs run on FBB because it folds cleanly, scores well, and costs less than SBS without a dramatic drop in print quality.
CRB / WLC (coated recycled board and white-lined chipboard)
Built from recycled fibre with a clay-coated white top liner, CRB and WLC trade a small amount of print fidelity for a genuine recycled-content story. Greyer core fibre can show through on lighter coating weights, so heavier coat weights or a double-lined structure are worth specifying if brand colours need to stay flat and consistent.
CUK / SUS (coated unbleached kraft and natural kraft)
Unbleached softwood kraft fibre gives CUK its characteristic warm brown tone and high tear strength, and one side is often clay-coated for printability while the reverse stays natural. It’s become the default for artisan food packaging, takeaway, and any brand leaning into an “unprocessed” aesthetic.
Chipboard/greyboard, C1S/C2S, and CCNB
C1S and C2S refer to coating on one side or two sides of any base stock, a spec detail rather than a separate material. CCNB (clay-coated news back) is a lower-cost recycled board with a coated print face, common in low-margin retail cartons where budget outweighs finish quality.
Corrugated (flute overview)
Corrugated isn’t paperboard, it’s a fluted core sandwiched between liners, and it belongs in the conversation because so many specification briefs confuse the two. DNPackaging’s material guide draws the same line: paperboard handles print and structure in a single sheet, corrugated handles impact and compression across a transit journey.
| Board type | Best for / typical use | GSM / caliper range | Ply structure | Print surface quality | Recyclability | Relative cost |
|---|---|---|---|---|---|---|
| SBS | Cosmetics, pharma, premium retail | 200gsm | Single or multi-ply, bleached virgin fibre | Excellent, best foil/emboss response | Recyclable, virgin fibre | High |
| FBB | FMCG folding cartons | 200gsm | Multi-ply, bleached outer/mechanical core | Very good | Recyclable | Medium |
| CRB/WLC | Recycled-claim packaging | 250gsm | Multi-ply recycled core, clay-coated liner | Good, some show-through risk | High recycled content | Medium/low |
| CUK/SUS | Craft, food-service, kraft branding | 150gsm | Single or duplex, unbleached kraft | Good on coated face | Recyclable, often unbleached | Medium |
| Greyboard/chipboard | Rigid boxes, inner supports | 800gsm | Multi-ply recycled, uncoated | Poor, used uncovered or laminated | High recycled content | Low |
| Corrugated (E/B/C flute) | Transit, e-commerce shipping | Varies by flute, not GSM | Fluted core between two liners | Fair, print usually on liner | Recyclable | Low/medium |
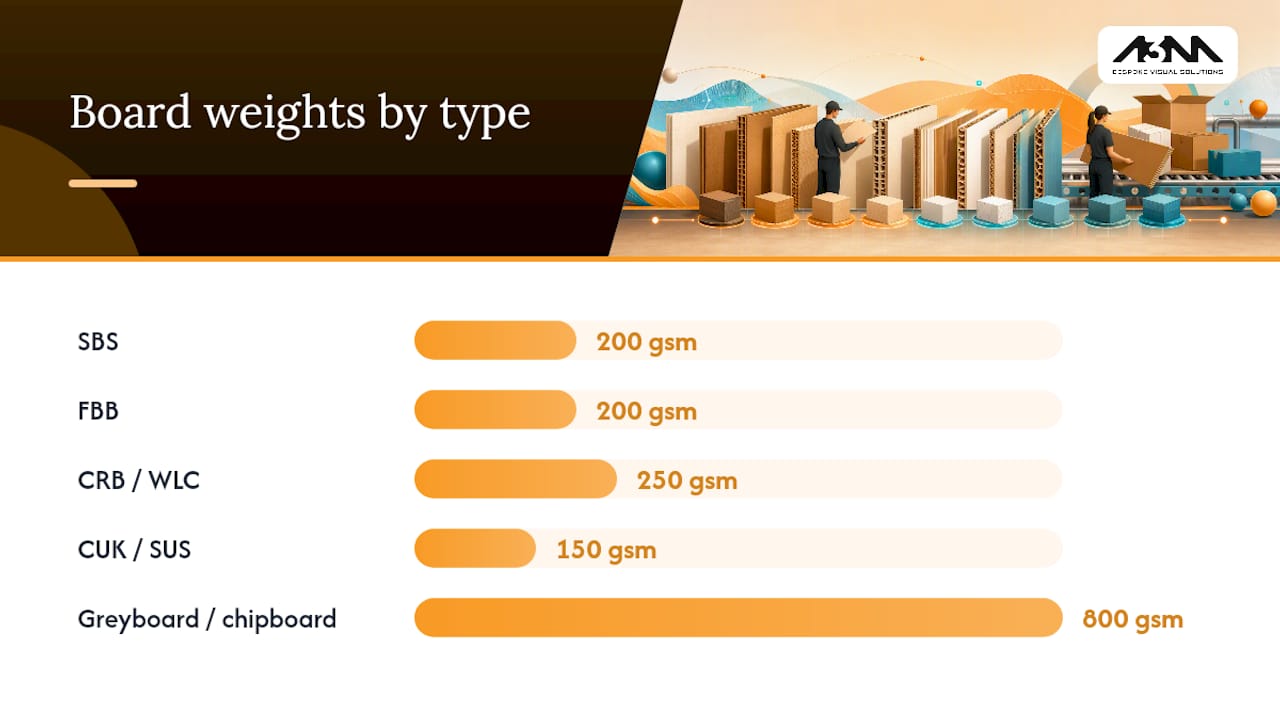
What technical specs actually define a board grade?
Grammage, expressed in grams per square metre, is the standard weight measurement, but weight alone doesn’t tell you how a board behaves on a converting line. Caliper, the physical thickness measured in points or micrometres, matters more for stiffness and fold performance because two boards at identical GSM can feel completely different depending on fibre bulk and ply count. Multi-ply construction adds rigidity without adding proportional weight, which is why FBB often outperforms a heavier single-ply board on shelf stiffness.
Stiffness, tested via Bendtsen or Taber methods, predicts how a carton resists crushing on a retail shelf. Burst and edge crush values matter more for corrugated shipping cases than for folding cartons, since they measure resistance to compression during stacking and transit. Surface gloss, opacity, and brightness govern how colour reproduces once ink hits the sheet.
- Higher GSM: greater stiffness and shelf presence, but higher material cost and more gluing pressure required
- Higher caliper at the same GSM: better fold memory, useful for hinged lids and rigid box walls
- More plies: added rigidity without proportional weight gain, though ply delamination risk increases
- Higher brightness/opacity: cleaner colour reproduction, particularly noticeable on process colour artwork
How do you choose the right packaging board?
Work through the brief before you touch a supplier quote.
- Define the product’s weight and fragility. Heavier or fragile contents need higher caliper or a corrugated outer, not just a heavier paperboard.
- Confirm the packaging’s function. Retail shelf presence calls for print fidelity; transit calls for compression resistance.
- Set the finish and print fidelity target. Foil, embossing, and fine screens point towards SBS or FBB; recycled claims point towards CRB or WLC.
- Fix sustainability requirements. Decide whether FSC chain-of-custody or a specific recycled-content percentage is contractually required before quoting.
- Set budget and run length. Short runs tolerate higher unit costs; long runs justify tooling investment in a premium grade.
- Check converting constraints. Confirm your die-cutter and folder can handle the caliper and ply structure you’re specifying.
When you brief a supplier, ask directly:
- What’s the minimum order quantity at this caliper and GSM?
- Which coatings and laminations are compatible with this base stock?
- Can you supply food-contact certificates for this grade?
- What’s the typical lead time and cost band for this specification?
Watch for quotes that specify caliper without GSM (or vice versa) with no cross-reference, no stated tolerance range, or vague sustainability claims with no certificate attached. Those gaps tend to surface as disputes later in production, and board grade selection genuinely does affect press behaviour and cost right through the production chain, not just at the point of purchase.
Which finishes suit which board type?
Clay coating, aqueous varnish, UV coating, lamination, cold foil, hot foil, and soft-touch finishes all behave differently depending on the base stock. SBS accepts foil and embossing with minimal show-through and holds fine dot detail well, because its bleached surface gives even ink absorption. CRB can suffer patchy foil adhesion if the coating weight is thin, since recycled fibre underneath can telegraph through. FBB sits between the two, handling most finishes competently without SBS’s premium cost.
Press behaviour also shifts with substrate: absorption rates and dot gain differ between coated and uncoated stock, which affects how CMYK colour reproduces on the finished sheet. Litho-lamination, printing on a thin sheet then bonding it to a rigid board, is often the better route for high-fidelity jobs that need a heavier caliper than a single sheet can carry economically. Our own guide to print quality and brand perception covers how finish choice changes shelf impact in more depth.
Pro Tip: Always insist on a press proof on the actual nominated board and finish, not a bench proof on a different stock. Colour and foil adhesion can shift noticeably between substrates, and a proof on the wrong sheet will mislead your approval process.
How sustainable are different packaging boards?
Recycled-content boards like CRB and WLC generally sacrifice a degree of brightness and stiffness compared with virgin fibre grades such as SBS and FBB, but the gap has narrowed as coating technology has improved. Buyers increasingly want documentation, not just a logo. Ask for FSC or PEFC chain-of-custody certificates and a stated recycled-content percentage on the invoice itself, not just printed on the carton.
Regulatory pressure is also reshaping component choices: UK government restrictions on single-use plastics increasingly affect plastic display windows and laminates on cartons, pushing specifiers towards water-based coatings or fully paper-based window alternatives.
- FSC/PEFC certificates should specify chain-of-custody status, not just membership
- Recycled-content claims should state a percentage, not just “recycled” on the pack
- Water-based coatings and paper windows are increasingly viable substitutes for plastic components
Procurement teams are asking for that paper trail more often than they used to, and buyers increasingly expect documented recycled-content evidence rather than a simple label claim on the finished pack.
What are typical GSM and caliper ranges by board type?
Specification ranges vary by mill and market, but the figures below give a workable starting point for quoting and comparison. Supplier tolerances typically run at plus or minus a few percent on GSM and caliper, so always confirm the exact tolerance band before locking a spec.
Trade sources commonly recommend a caliper range of roughly 18 to 24pt for premium folding cartons, which lines up with mid-to-upper SBS and FBB specifications. Points and micrometres both describe the same physical thickness; converting between the two matters when comparing a UK mill’s caliper figure against a European supplier quoting in microns. Small-run orders often carry a minimum caliper or GSM step, since mills batch-produce at fixed thicknesses rather than custom-run every order.
What converting constraints affect board choice?
Die-cutting, scoring, and folding tolerances tighten as caliper increases, and high-GSM boards slow down press and finishing lines because they need more dwell time to score cleanly without cracking. Glueing and heat-setting also become less forgiving on heavier stock, since adhesive needs longer to cure across a thicker joint.
- Confirm scoring tolerances with your converter before finalising artwork on anything above 18pt
- Expect slower machine speeds on greyboard and heavy multi-ply SBS compared with standard FBB
- Special finishes like foiling or soft-touch lamination add production days, so factor that into lead time
Pro Tip: Run a short pre-production sample, even just 50 to 100 units, before committing to a full print run. It’s the cheapest way to catch a scoring or folding fault before it becomes a warehouse full of unusable cartons.
When should you bring in a packaging or print partner?
Call in a specialist supplier when a brief involves complex finishes, food-contact certification, tight structural tolerances on a rigid box, or when you need converting and fulfilment handled under one roof rather than split across vendors.
- Complex foil, emboss, or soft-touch finishes that need press proofs on the nominated stock
- Food-contact or pharmaceutical-grade certification requirements
- Rigid box or structural packs with low fold tolerance
- Projects needing fulfilment or multi-site distribution support
Ask any supplier for material samples, proofs on your actual chosen board and finish, engineering drawings with scoring dielines, and clarity on logistics or fulfilment capacity before you commit. Our breakdown of specification-grade print requirements covers what those engineering drawings should include in practice.
A manufacturer’s note on getting the spec right
The most common error we see isn’t picking the wrong board family, it’s under-specifying caliper while over-specifying finish. A brand asks for foil on a grade too light to hold it, and the rework costs more than the correct board would have. A half-point caliper increase, agreed before print, has saved entire production runs from cracking on the fold line.
How A3M supports packaging board selection and production
Getting the specification right on paper is one thing; getting it right off a live press is another, and that’s where in-house manufacturing removes a lot of the guesswork. A3M works from material sampling through to prototyping and litho-lamination, so you can see foil adhesion, fold behaviour, and colour on your actual nominated board before committing to a full run.
Beyond board selection, our finishing capabilities cover foiling, embossing, and specialist coatings across the SBS, FBB, and recycled grades this guide has covered, alongside project fulfilment and web-to-print support for businesses managing packaging across multiple sites. If you’re weighing up print manufacturing for a packaging or display project, our large format print manufacturing capabilities page sets out what an in-house production line can do for prototyping timelines and finish quality. Get in touch for a sample pack and a quote against your specific board and finish requirements.
Sources
- Gov
- Paperboard — Wikipedia
- Paper Stocks and Board Grades for Packaging: The Complete Guide - Crateform
- Paperboard packaging material — DNPackaging
Recommended
- Product packaging print explained for businesses – A3M
- Brochure paper weight: choose the right GSM for print – A3M
- Why specification-grade print matters for marketers – A3M